Oldbury UK

Oldbury UK, now the specialist engineering and defence products division within Boughton Engineering, is one of Britain’s leading specialist trailer, mobility and engineering solutions providers.

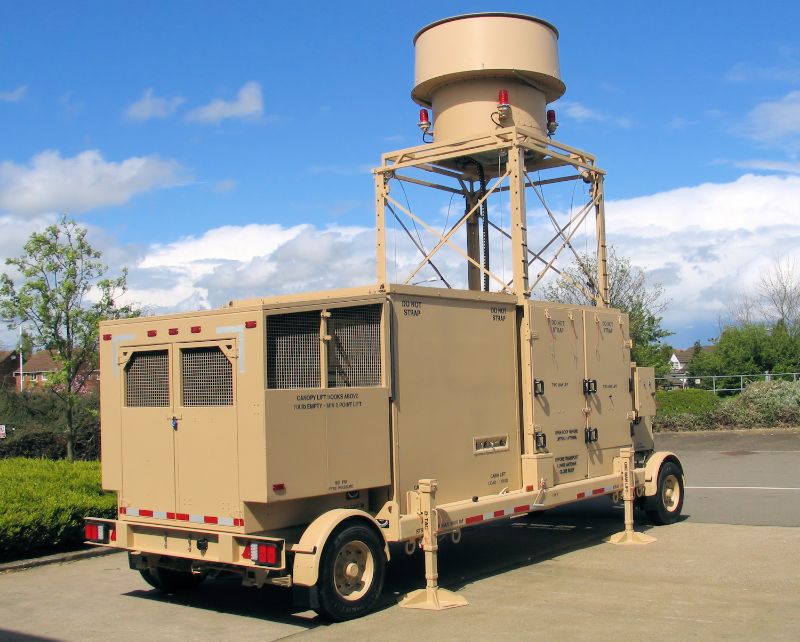
Its engineering capabilities include the design, development and manufacture, integration and supply of specialist trailers, transportable systems and carrier platforms from lightweight applications through to maximum weight special types.

It offers standard, bespoke and UOR (urgent operational requirements), mobility and engineered solutions for a wide range of sectors and industries worldwide.  These include defence, homeland security, CBRN (chemical, biological, radiological, nuclear) and aerospace.

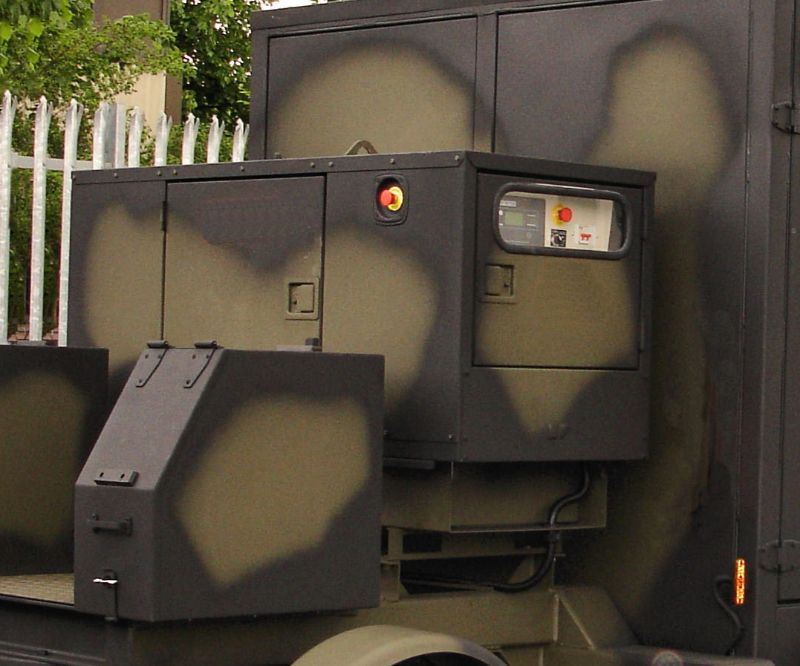
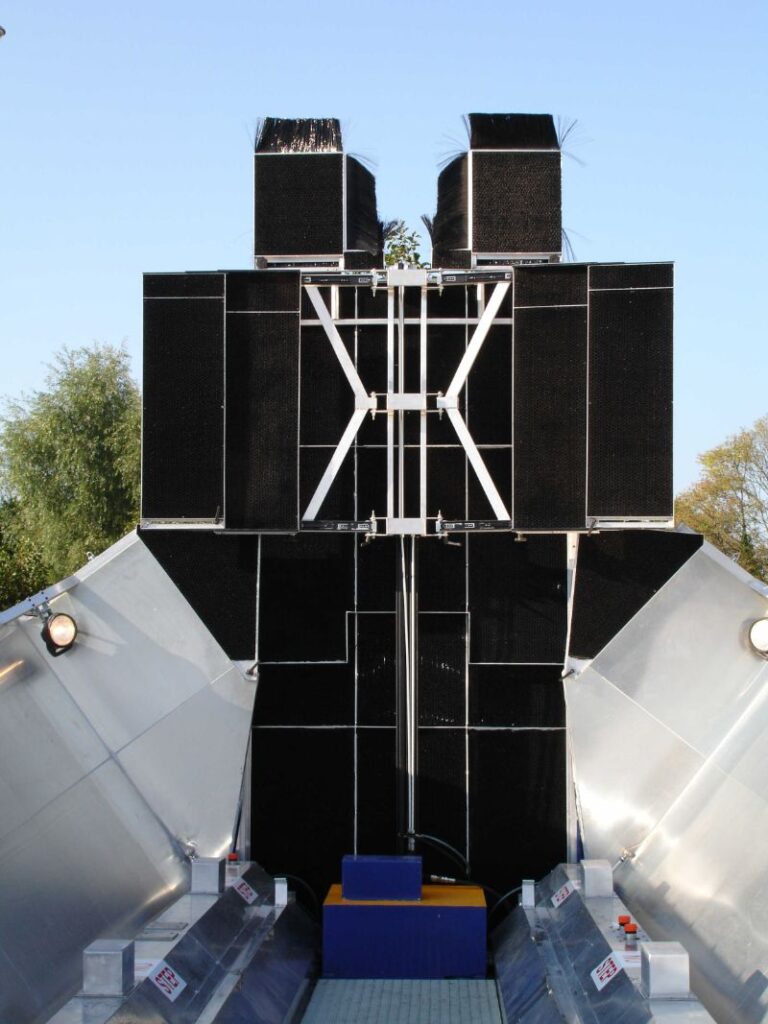
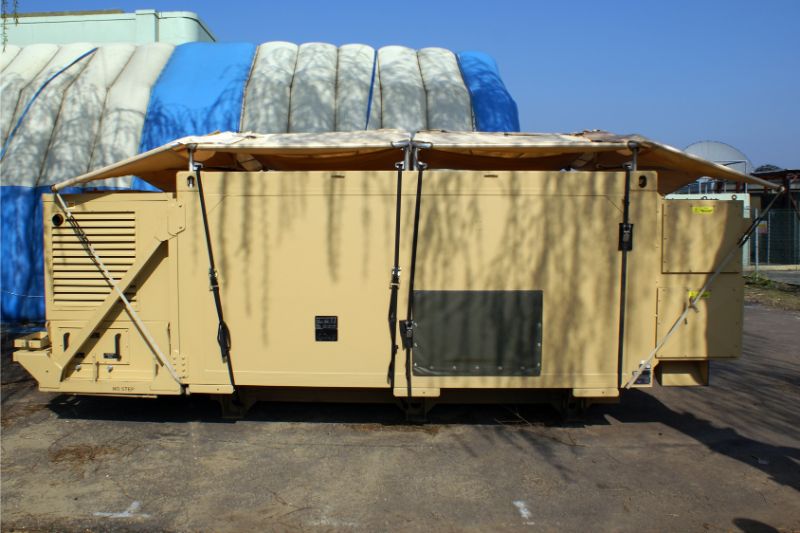
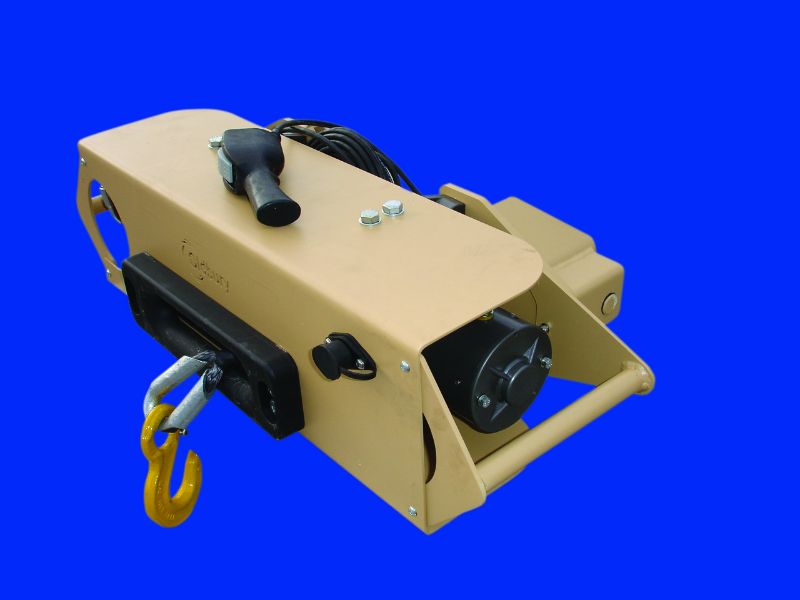
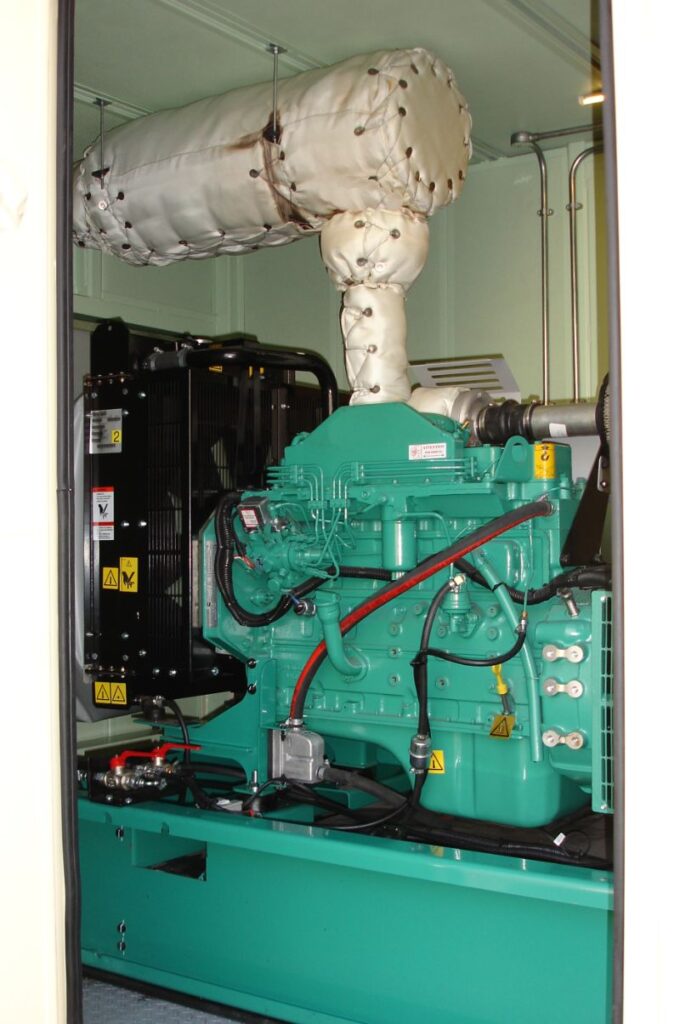
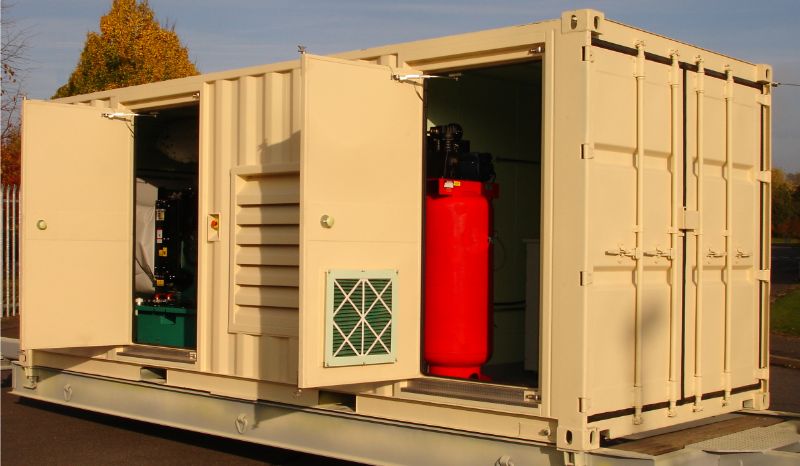
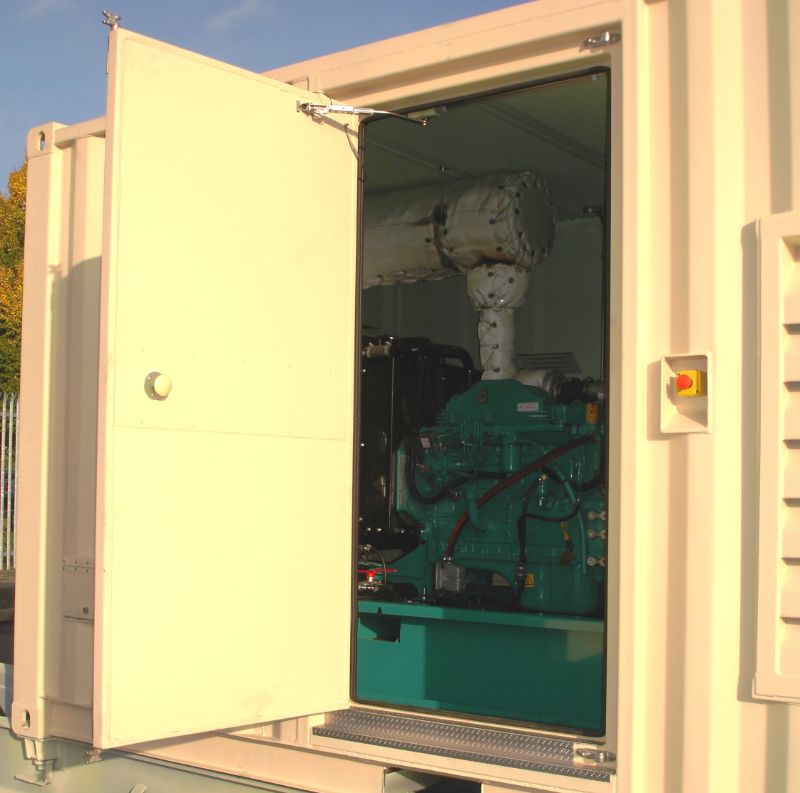
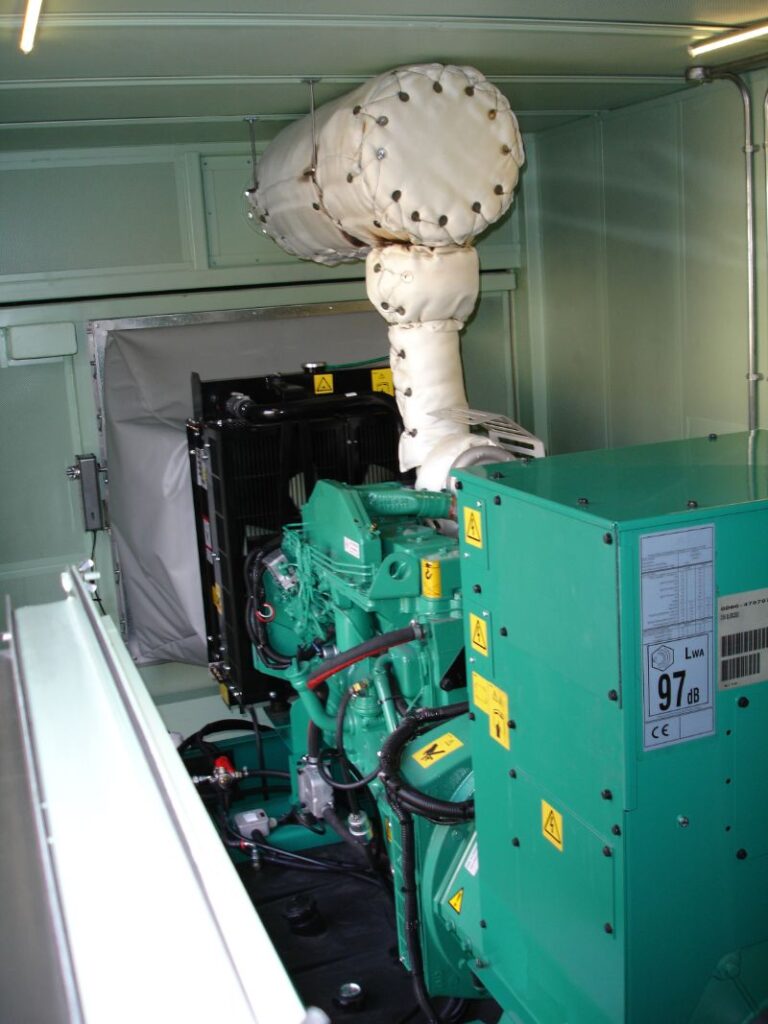
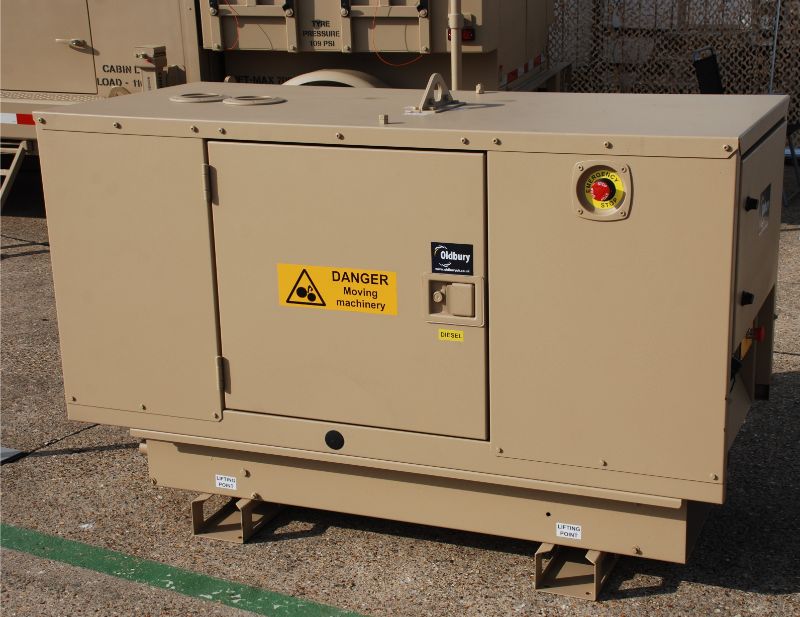
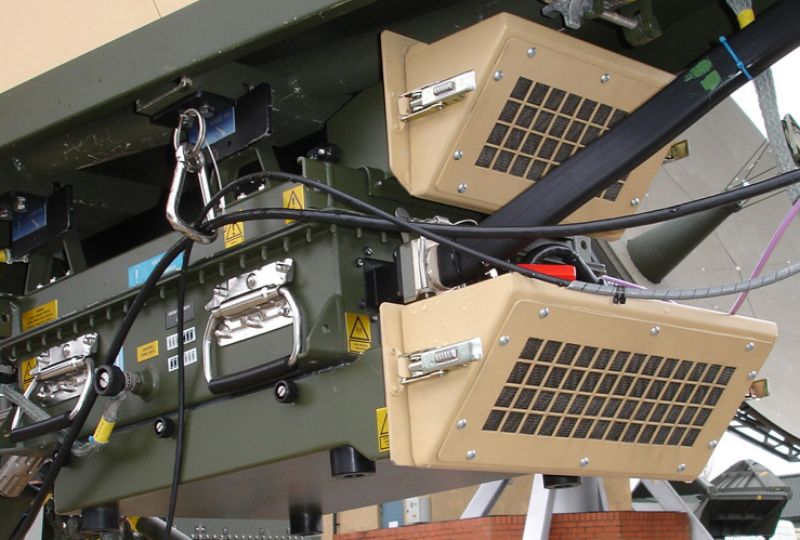
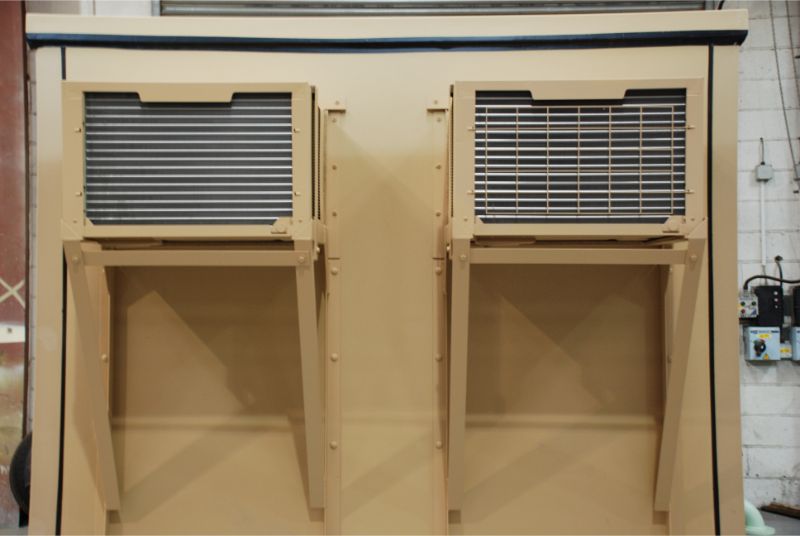
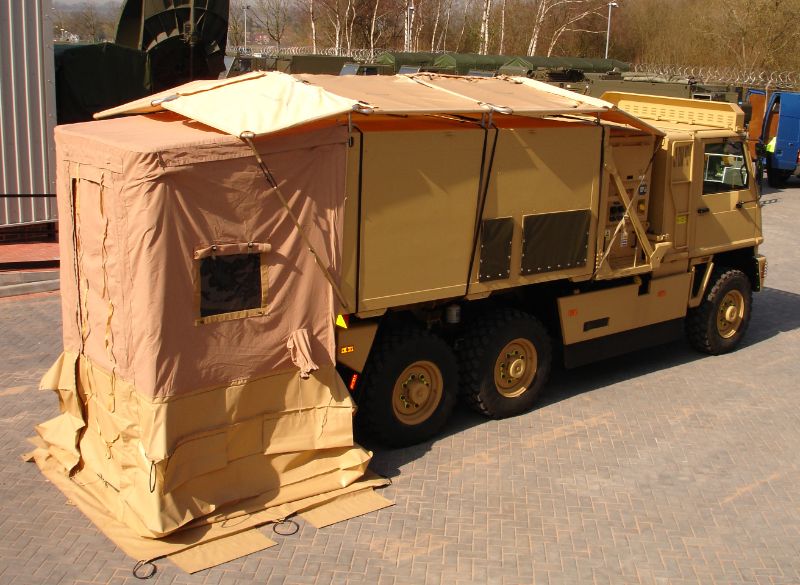
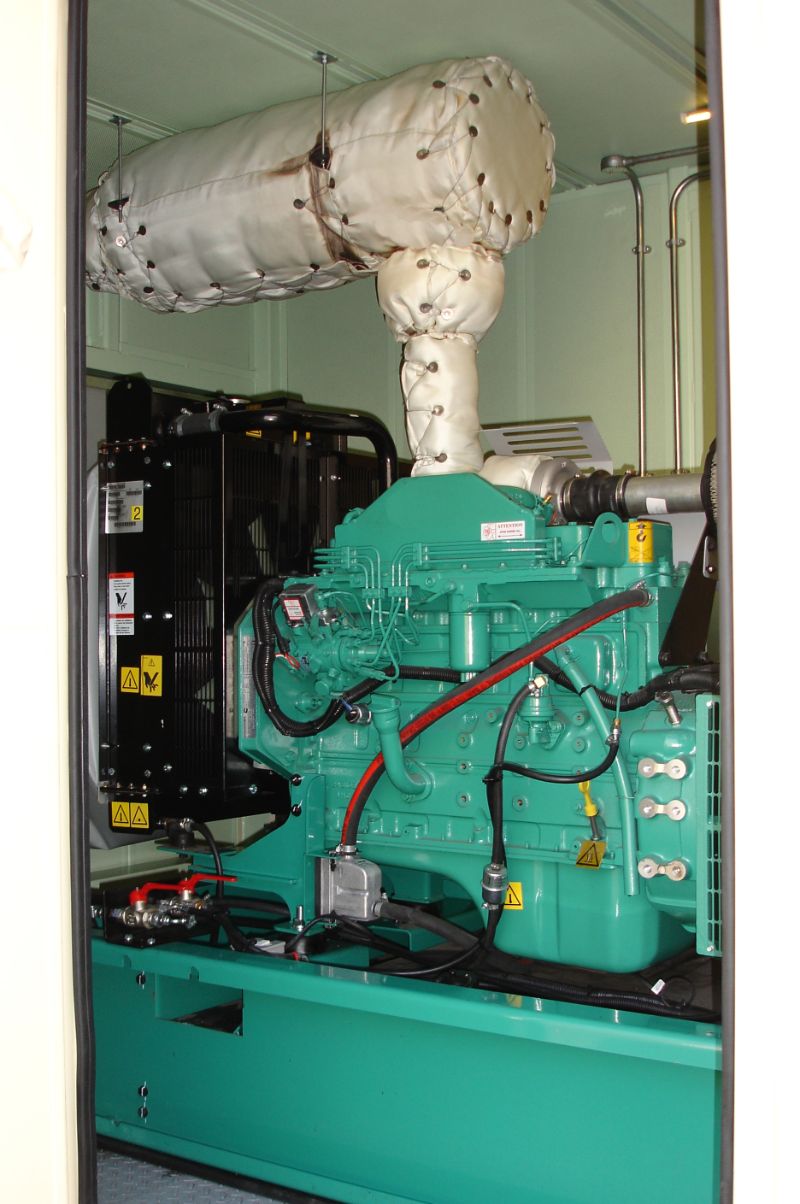
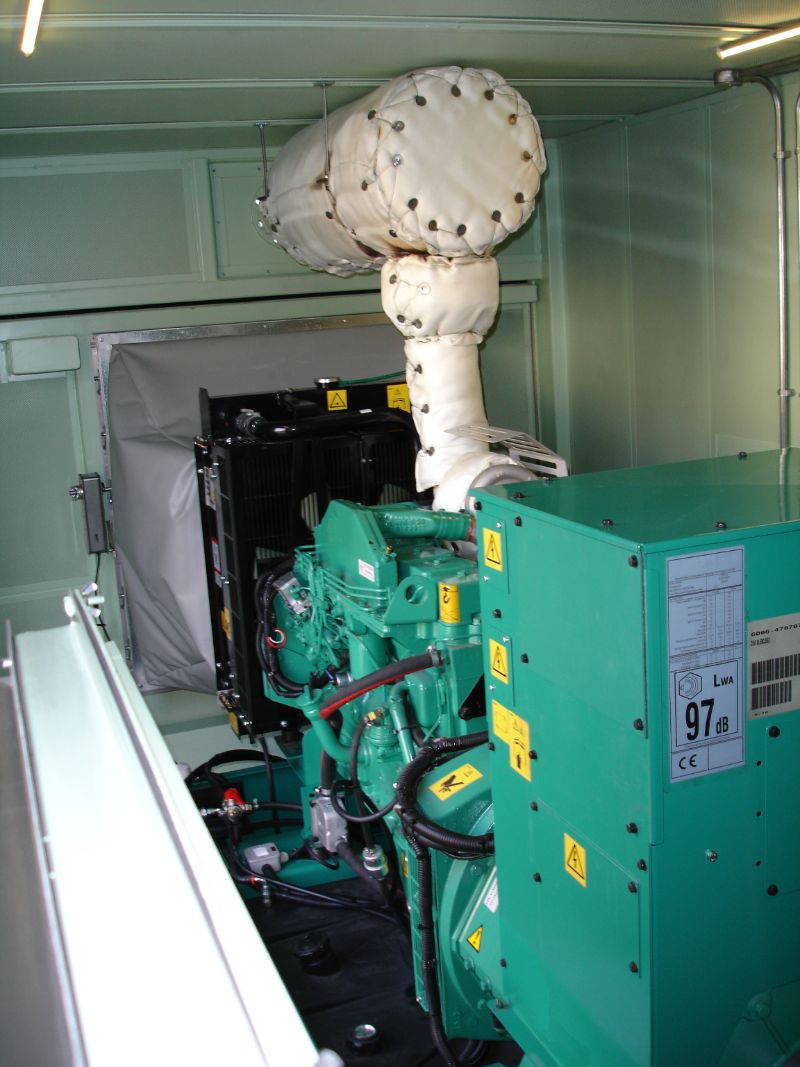
Its range of ruggedised ancillary equipment for theatre operations includes enclosed generator packages, high performance air-conditioning units, solar shields, environmental protection systems and a range of high free volume filtration packages.

It has also earned a reputation for being a solution provider… from innovative thinking, creative design, best practice engineering, manufacture and delivery to through life support.

The company’s approach is practical and pragmatic… it is about understanding operational needs – and engineering solutions.  Example projects and programmes for which Oldbury has designed, developed and delivered solutions can be divided into three basic categories:

More about Oldbury UK

Founded in 1861 by Isaiah Oldbury, supplying axles, suspensions and components for horse drawn carriages and carts, the company has been at the forefront of British engineering innovation and excellence for over 150 years.  It has been supplying specialist trailers, transporters and equipment to all three armed forces and civil agencies for more than 50 years.

It was acquired by Skan Group Holdings in 2000 and is today co-located within Boughton Engineering’s main headquarters facilities in the West Midlands.  Steady growth, coupled with significant investment and plans for future expansion, sees the company now operating across three sites, two of which are local and provide 3.5 acres combined, with 45,000 sq. ft. of enclosed production space.  These incorporate overhead craneage, extensive fabrication, erecting and fitting bays; surface treatment and paint shops, advanced CAD and design engineering capabilities, service and parts operations.  The third site is a dedicated modern fabrication facility in North Devon.  The company is fully accredited to TUV ISO 9001.

Boughton Engineering and Oldbury UK is a member of both ADS and NDI.
Defence & Homeland Security

Oldbury UK has an established reputation as a Tier supplier, specialist contractor and Partner of Choice in the defence and homeland security sector.  Particularly in the important area of UORs (urgent operational requirements), it has demonstrated its significant capability and flexibility in design, development, fabrication, manufacture, early delivery and support.
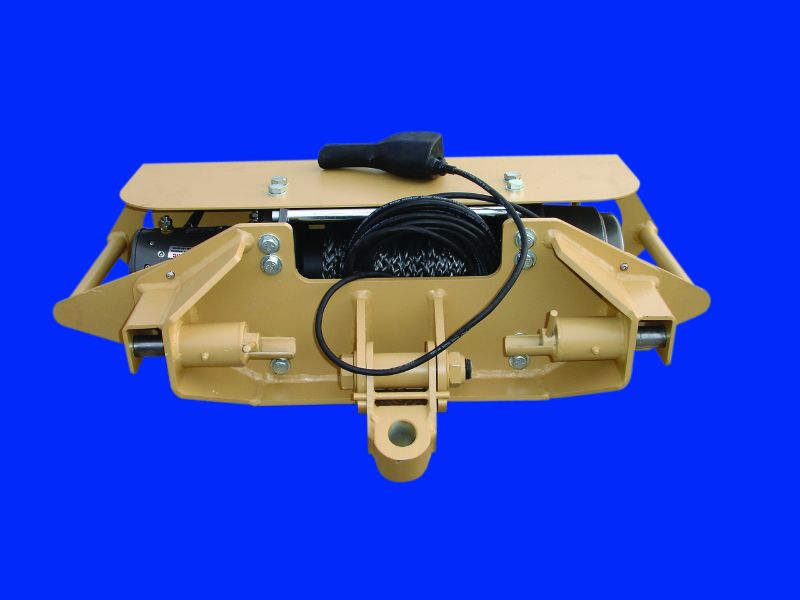
Oldbury provides mobility and engineered solutions for Primes, the supply chain and the end-user – and its organisational culture – as well as its engineering approach and experience are fully in line with the requirements and expectations of the sector.

The company is also closely involved with final assembly, systems integration and user support programmes – and is able to provide comprehensive through life support packages.  In addition, Oldbury provides ‘one stop’ engineering solutions for specialist ancillary equipment, in-service modifications or upgrades and other theatre climate and operational requirements.

Programmes for which Oldbury has provided engineered solutions include:-

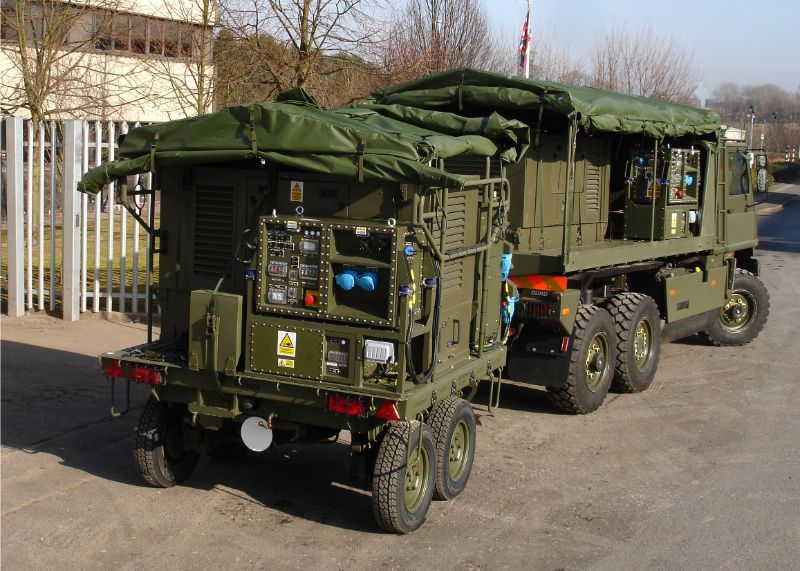
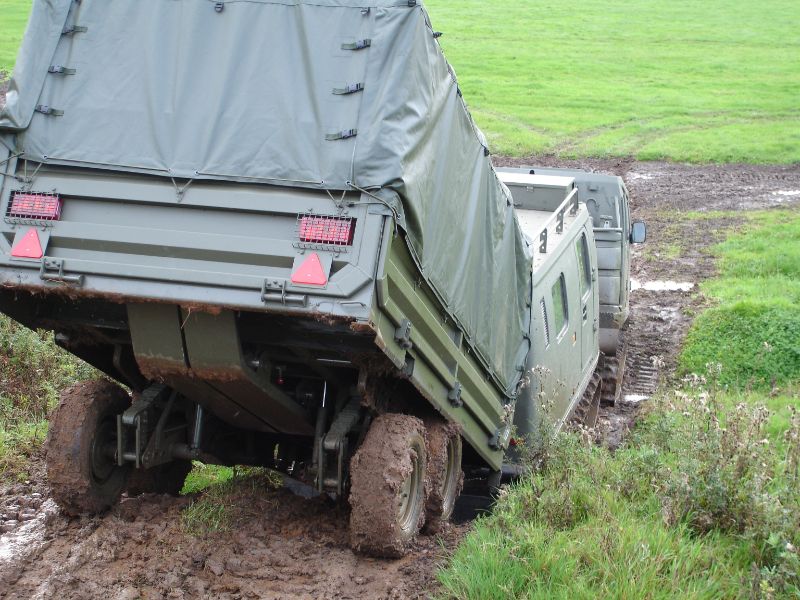
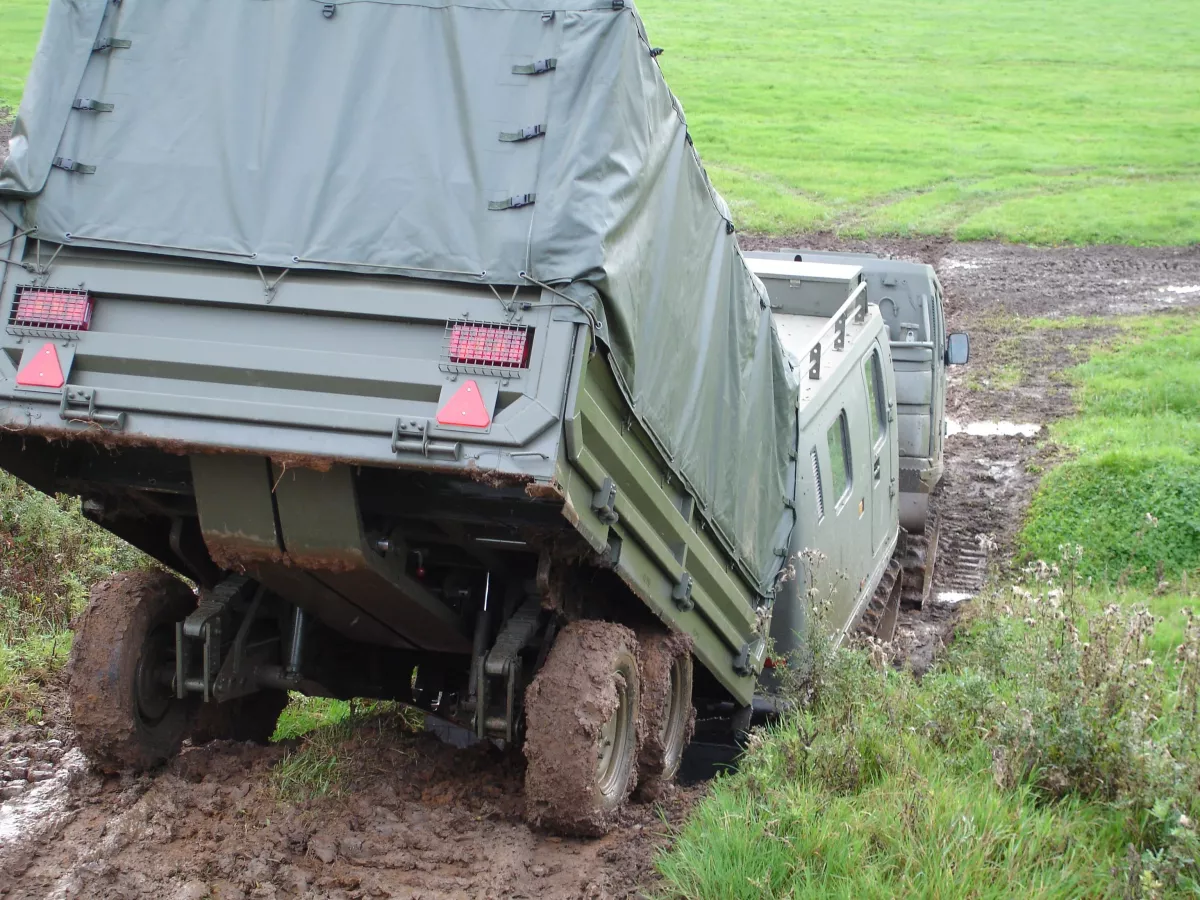
  • Multi-Role (MR) Off Highway Trailers
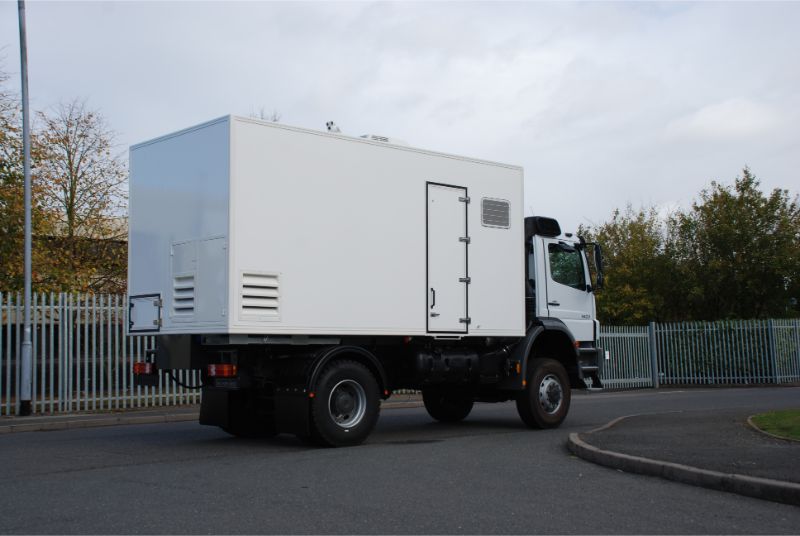
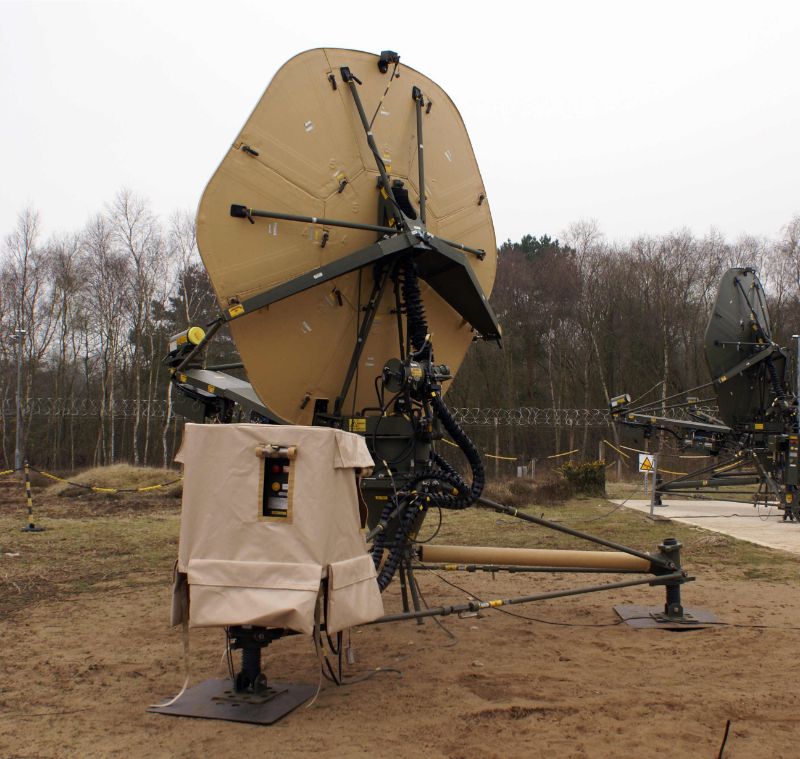
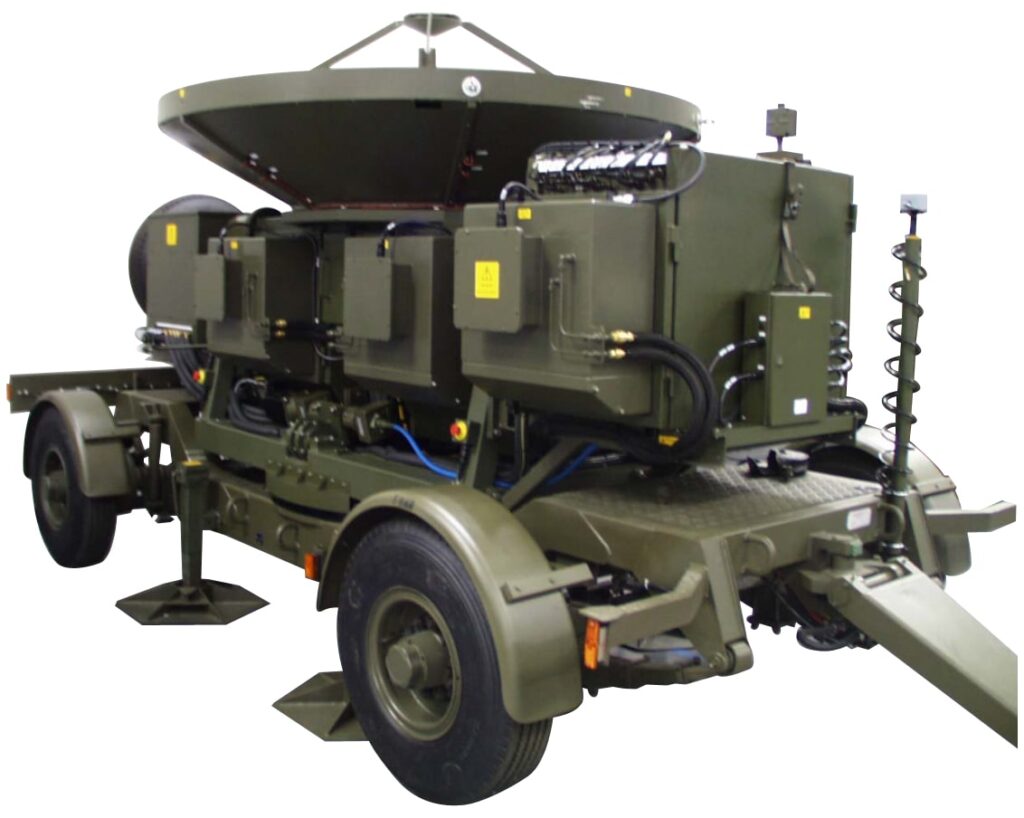
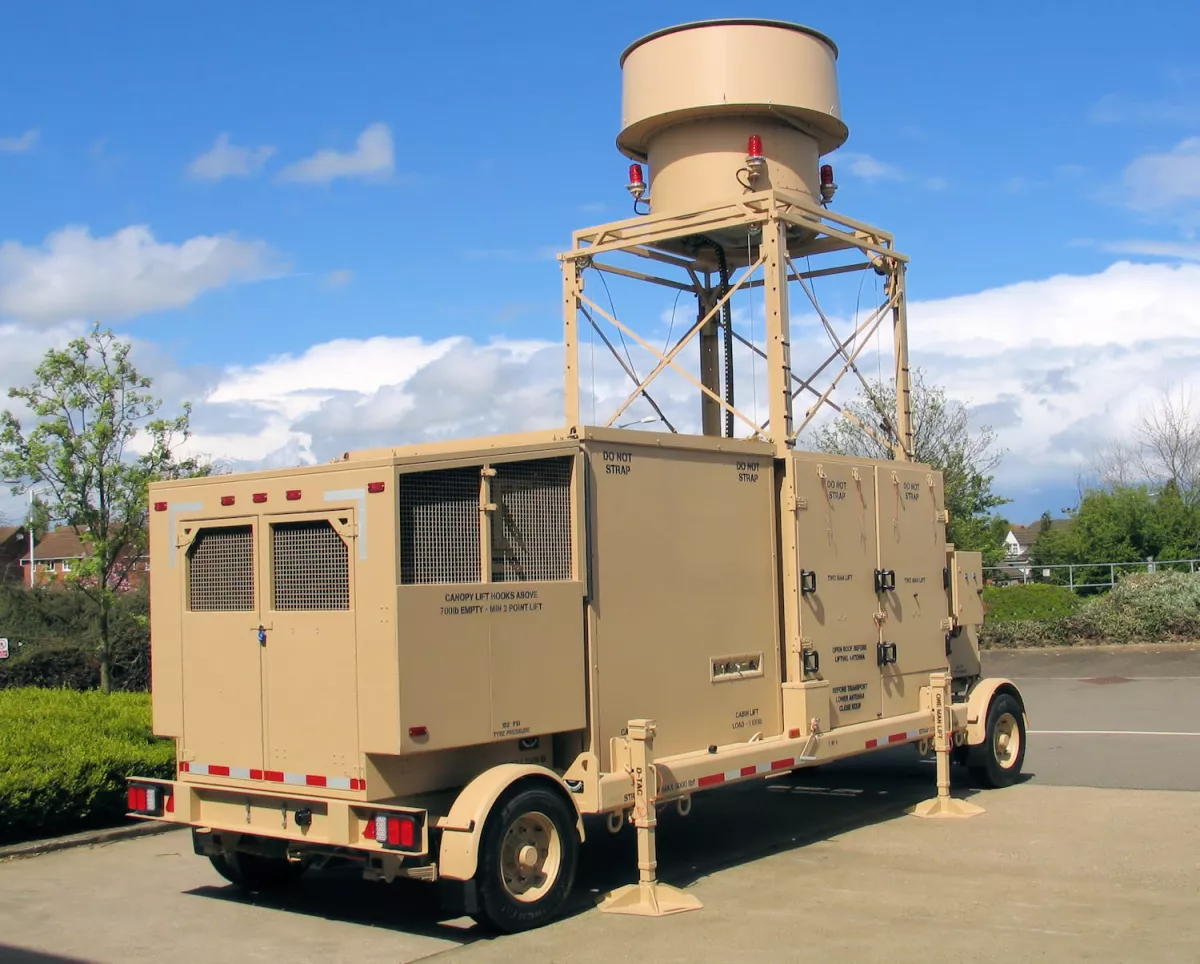
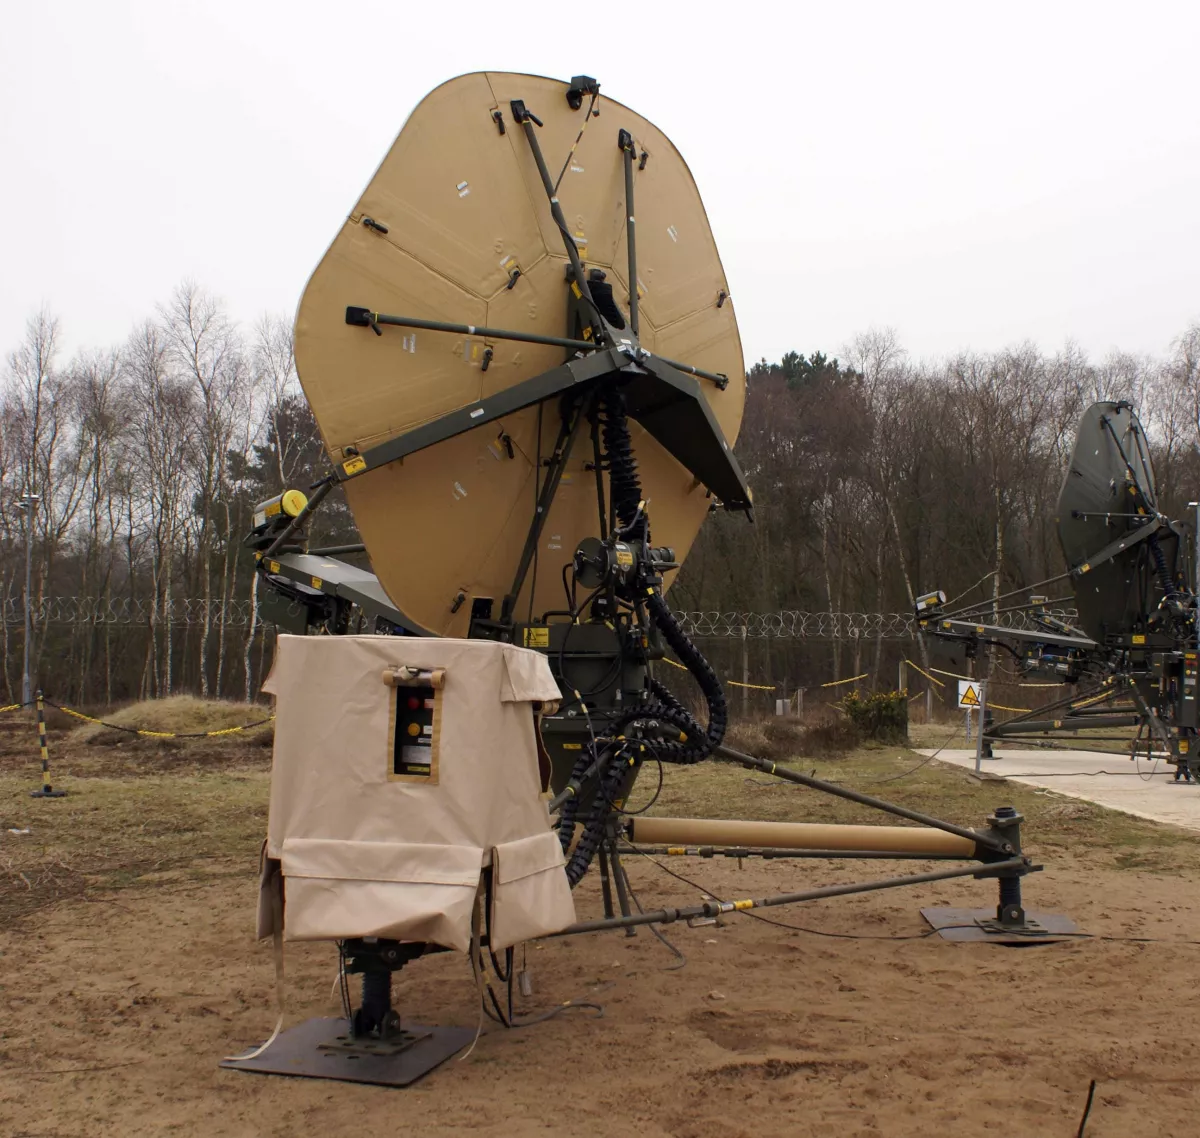
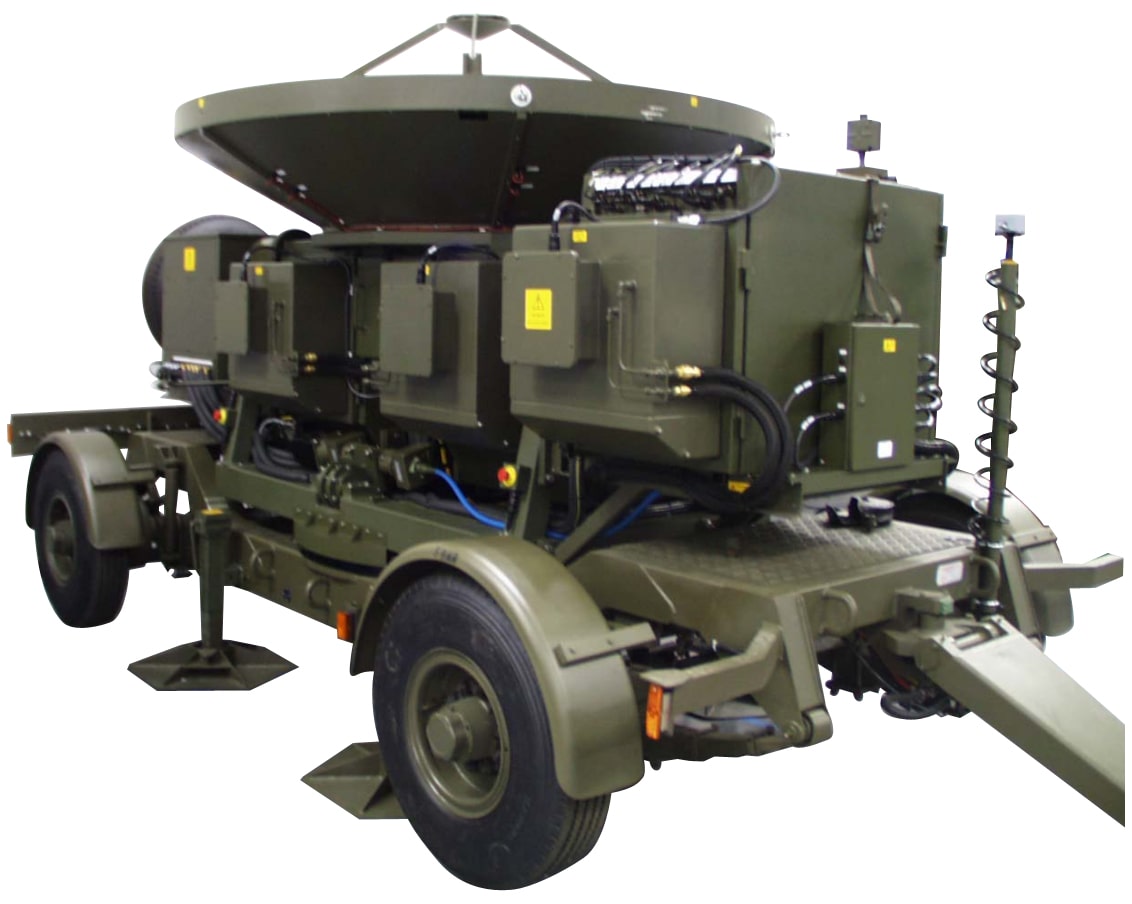
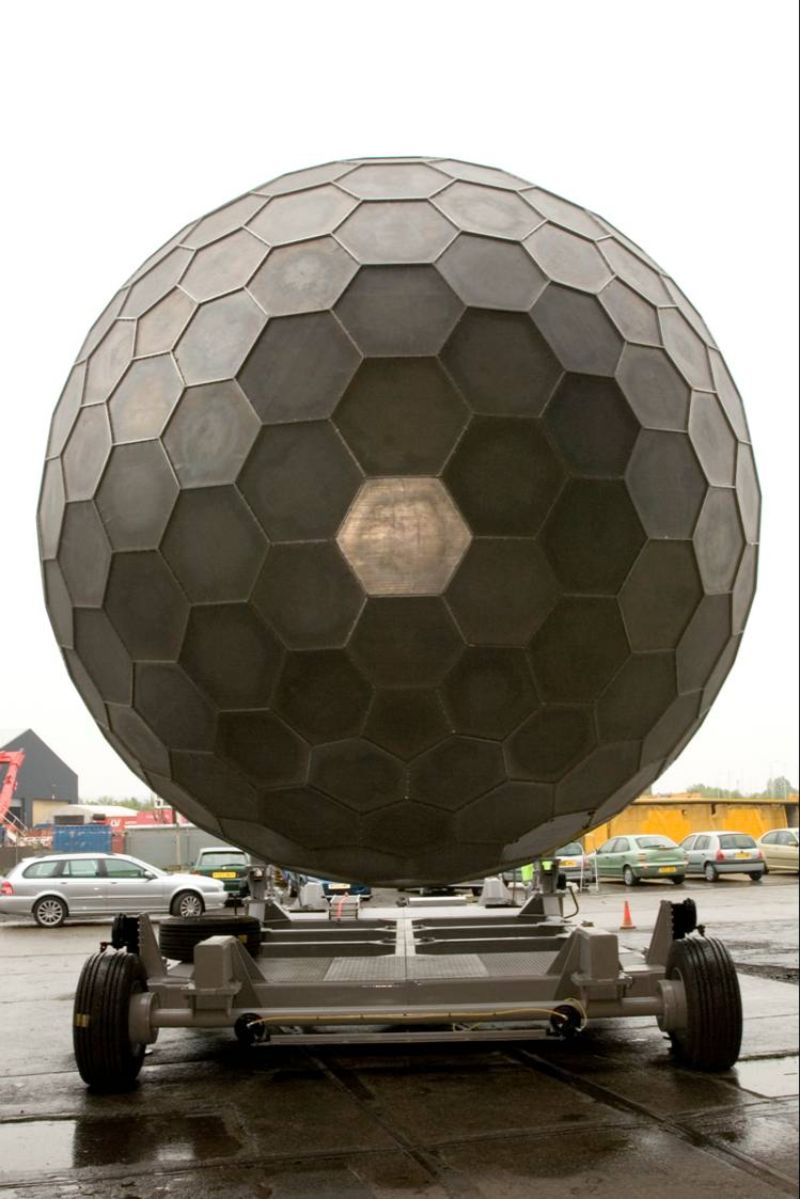
  • Mobile and Air-Portable Ground Stations
  • Satellite Receiver Platforms
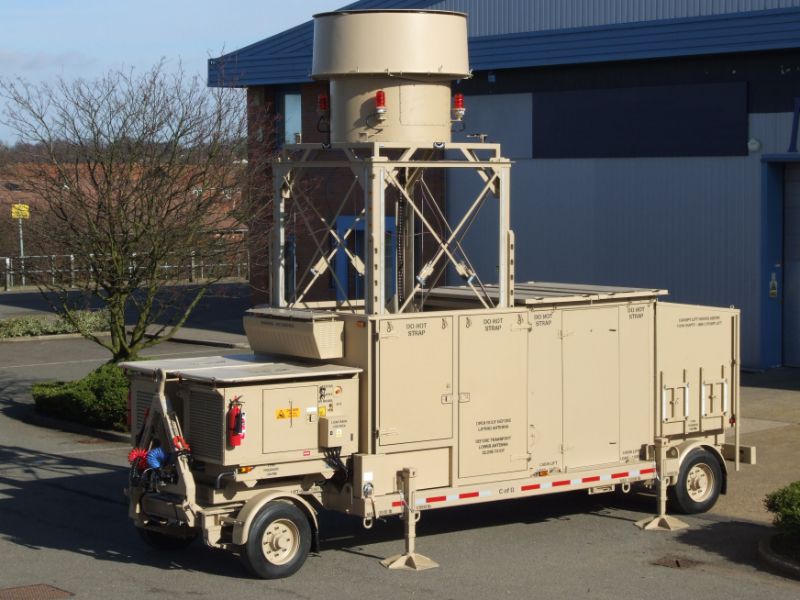
  • Mobile Tactical Air Navigation Platforms
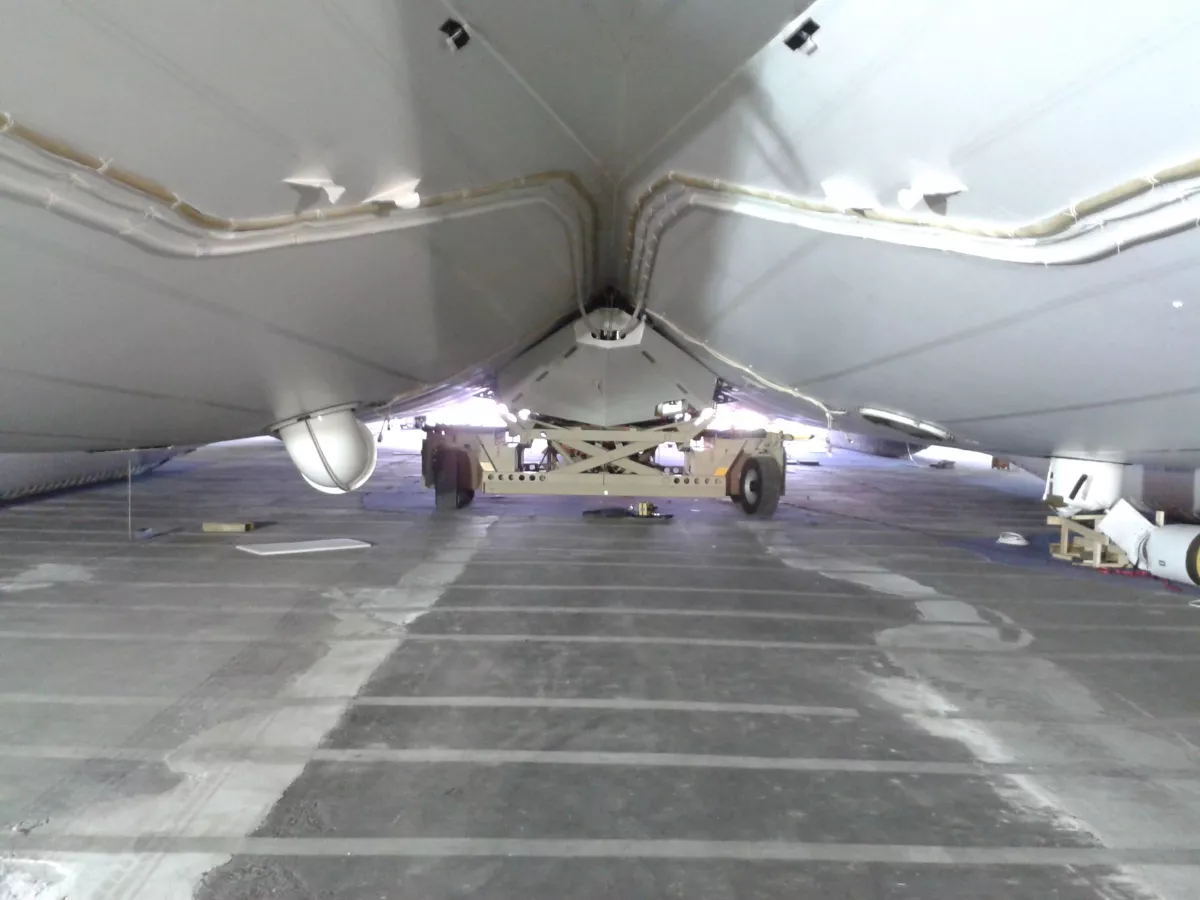
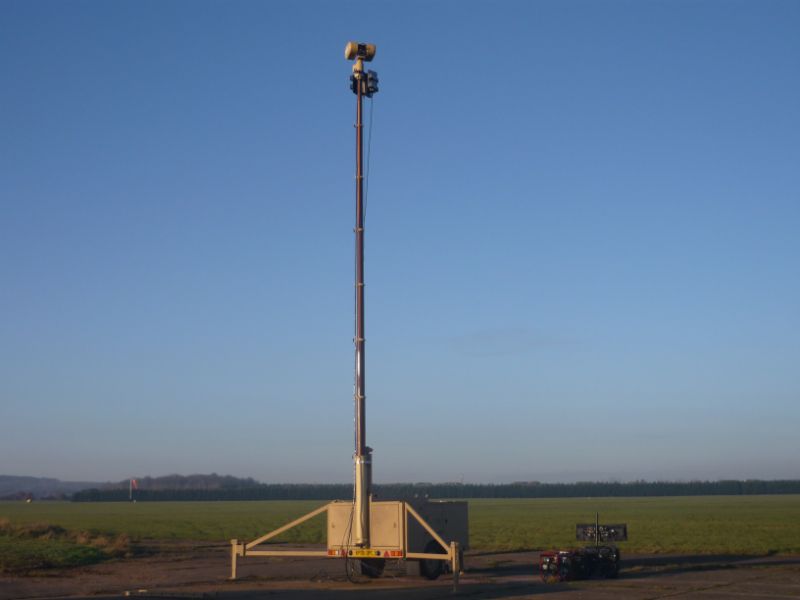
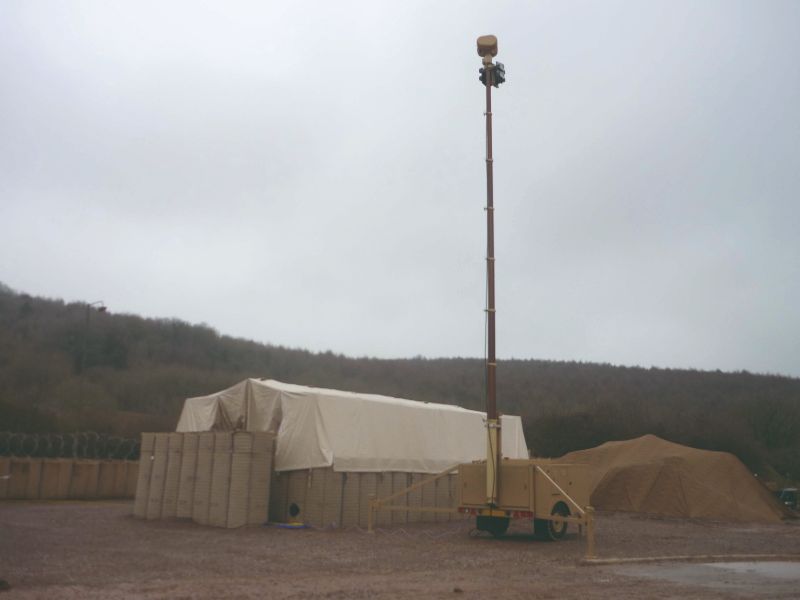
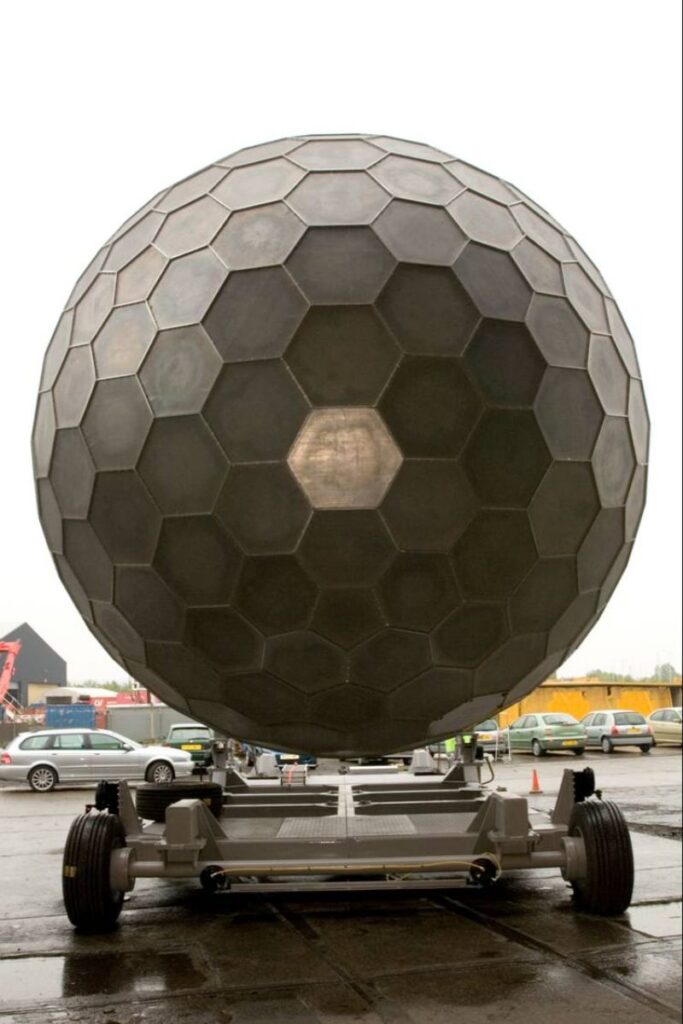
  • Wide Area Surveillance Platforms
  • Integrated Command & Control Units
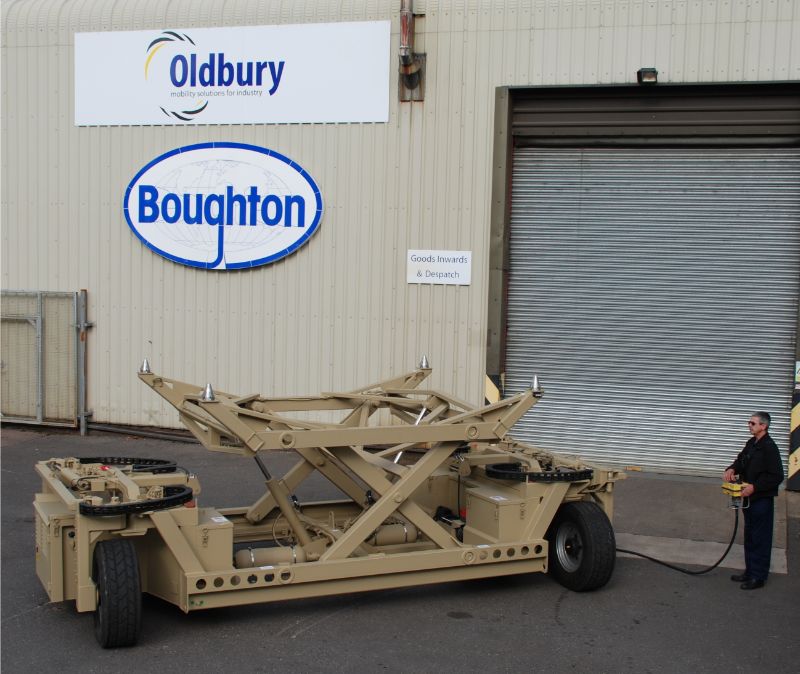
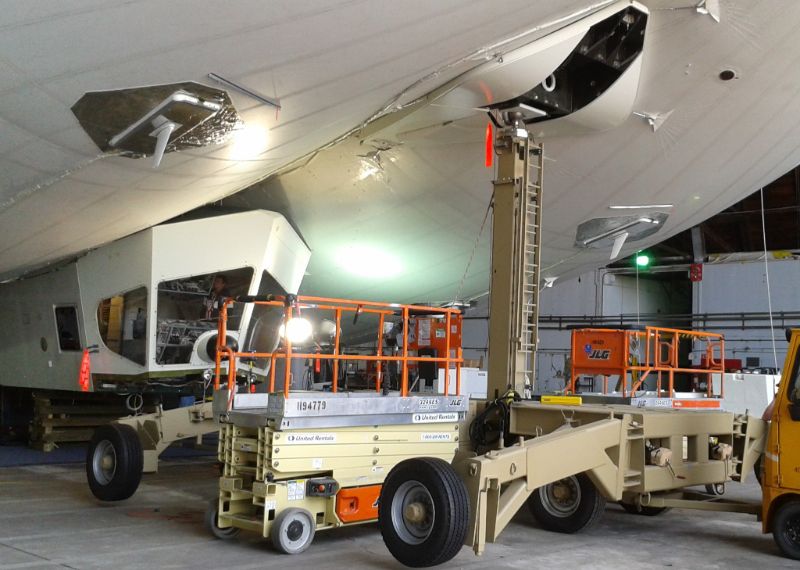
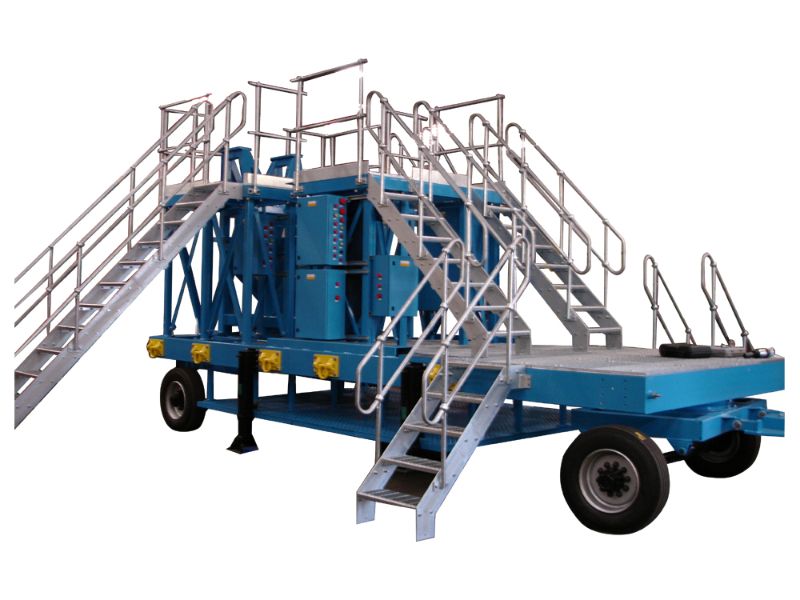
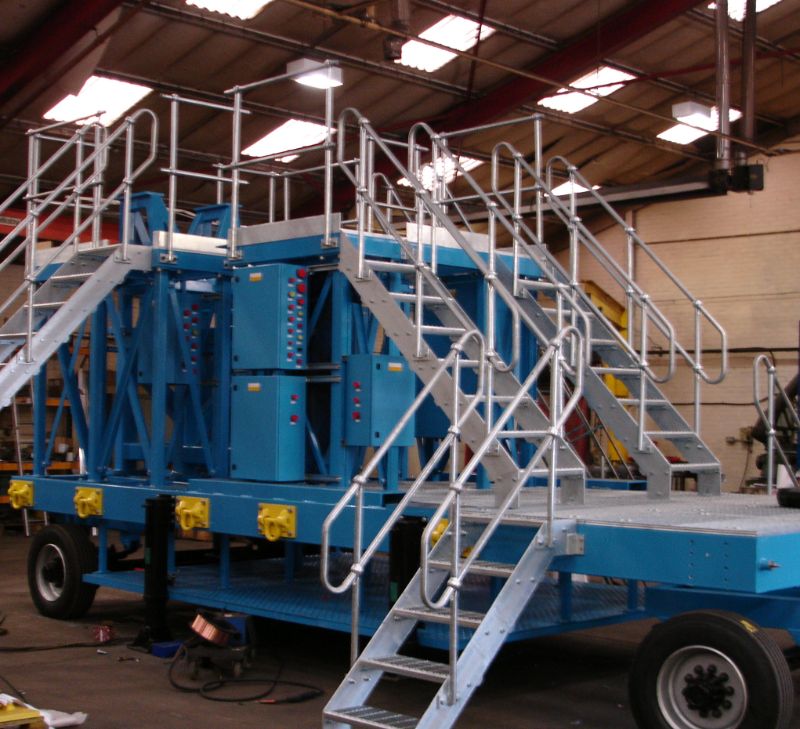
  • Equipment Servicing Platforms
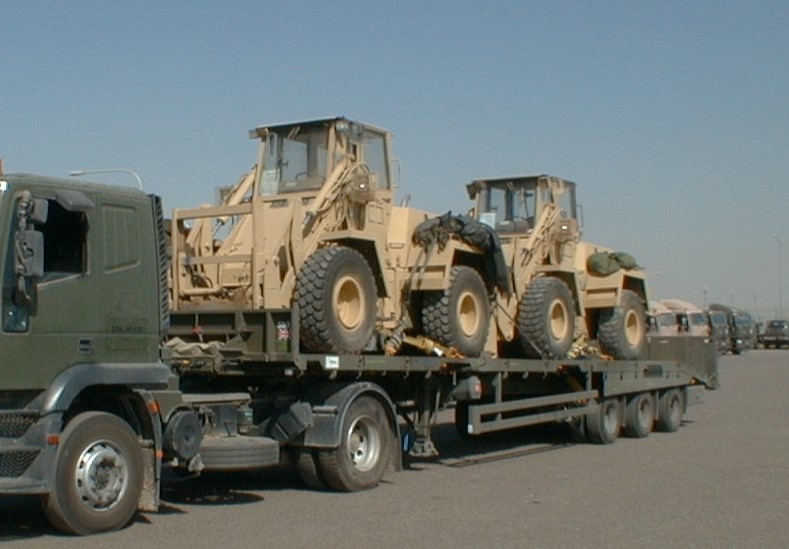
  • Sliding Bed Logistics Trailers
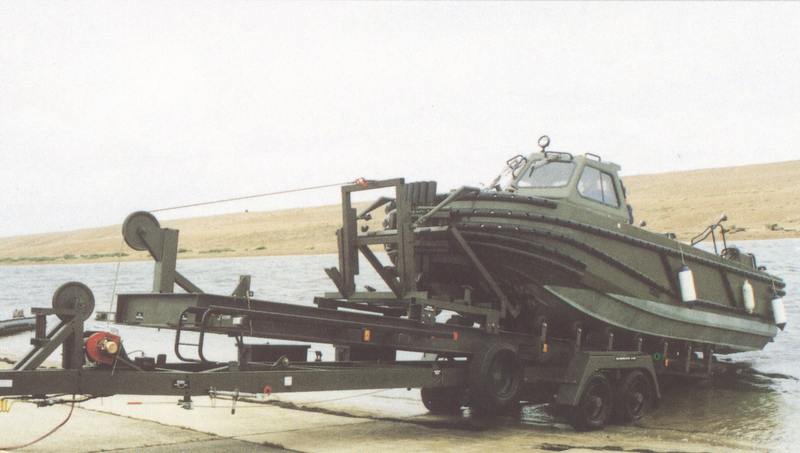
  • Combat Support Boat Trailers
  • Lightweight Centre-axle Trailers
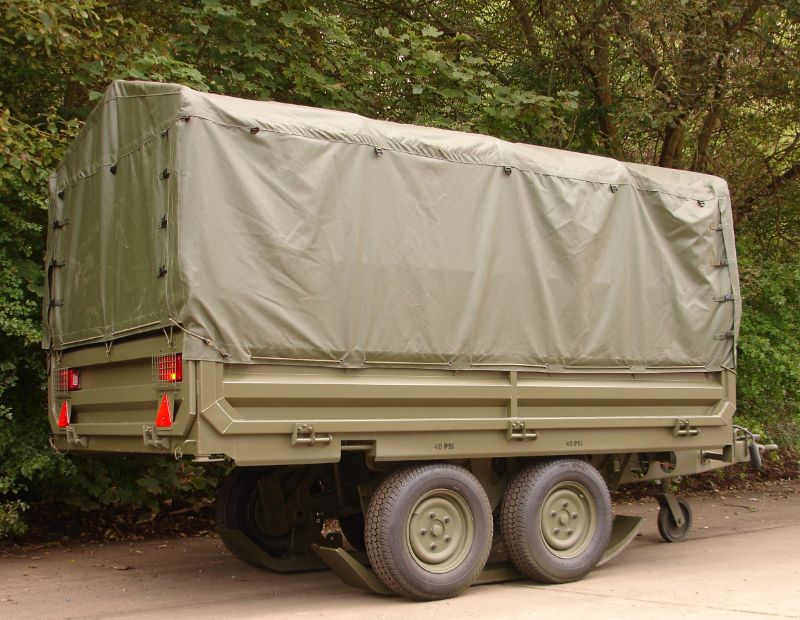
  • General Purpose Cargo Trailers
  • Ackerman Steer Communications Trailers
  • Special Purpose Trailers
  • Mobile Decontamination Systems
  • Mobile Vehicle & Equipment Wash Units

Specialist & Bespoke Trailers

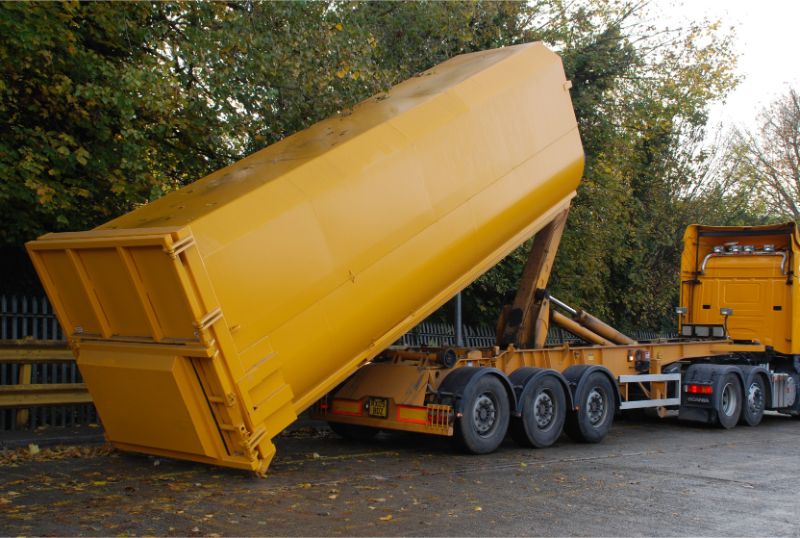
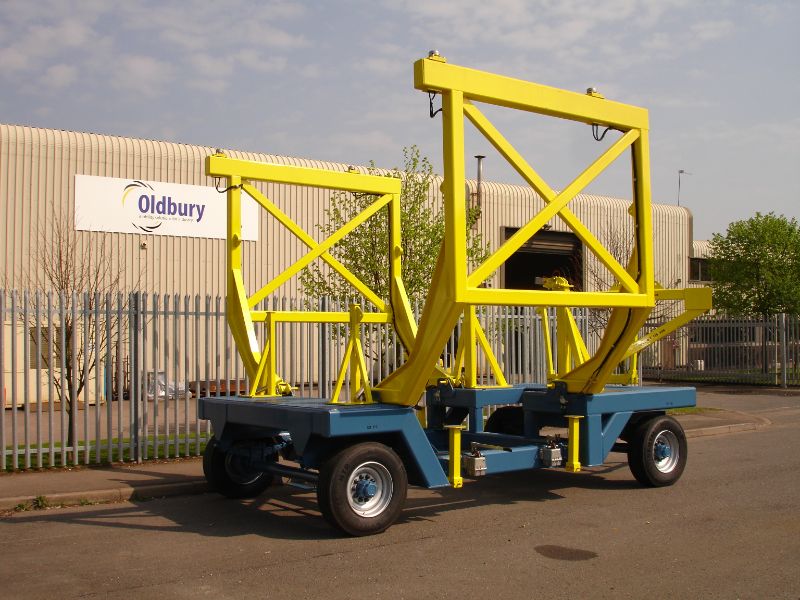
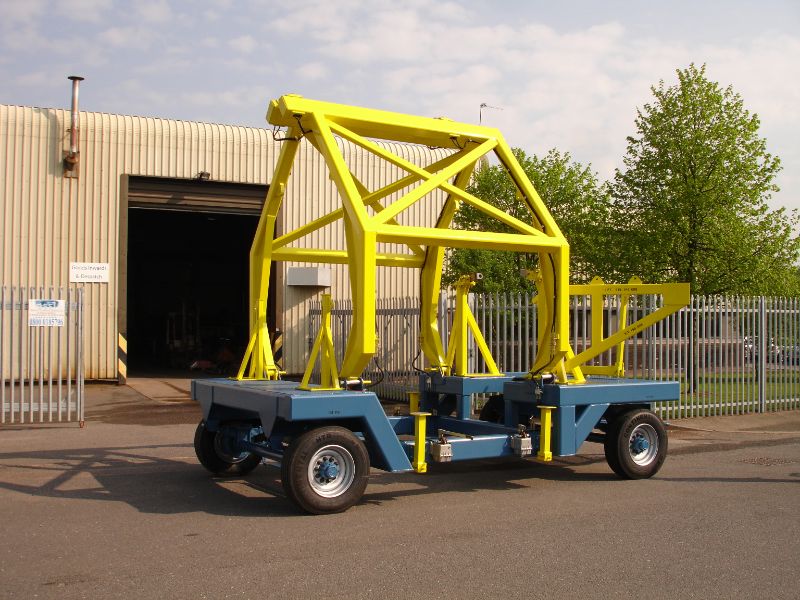
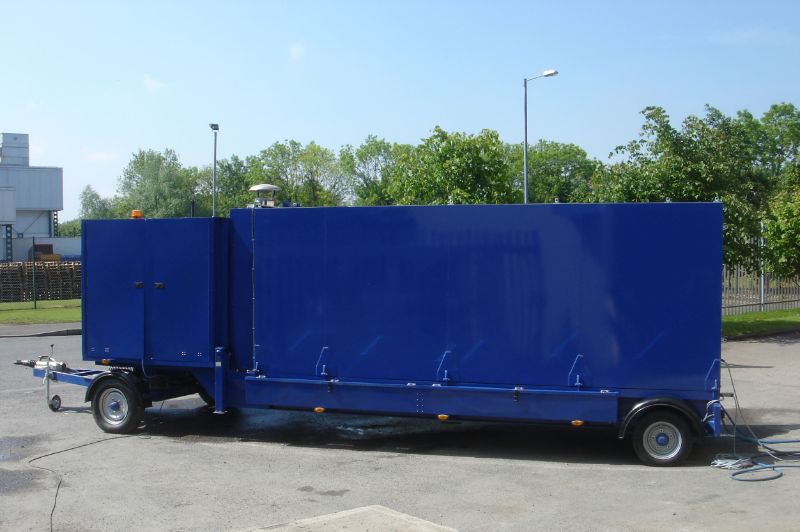
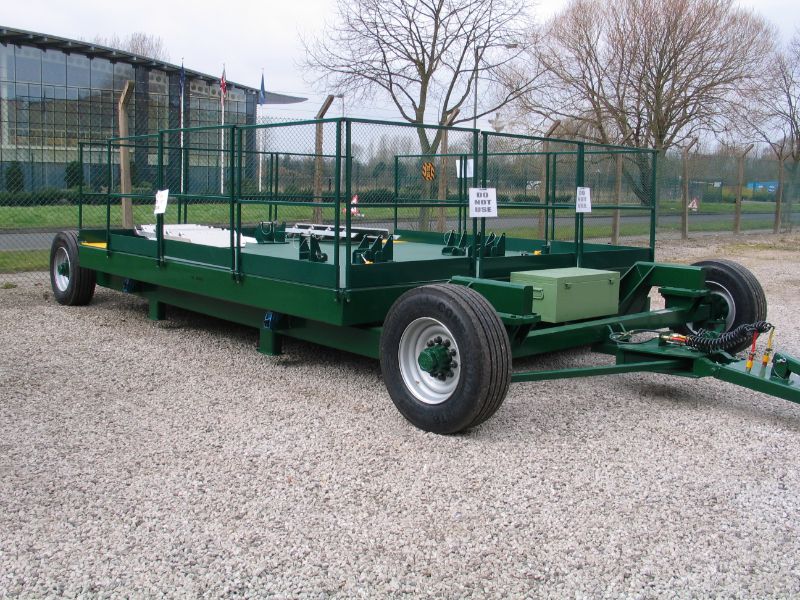
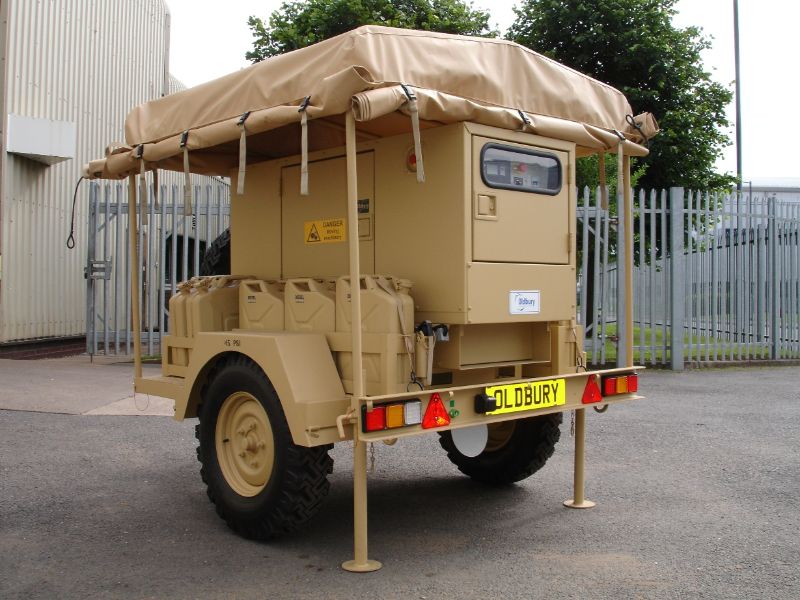
Oldbury UK has a proven track record for the design, manufacture and supply of a wide range of specialist, bespoke and purpose-built trailers to meet the requirements of all the market sectors and industries it serves.

Examples of these special requirements for which Oldbury has provided engineered solutions include:-

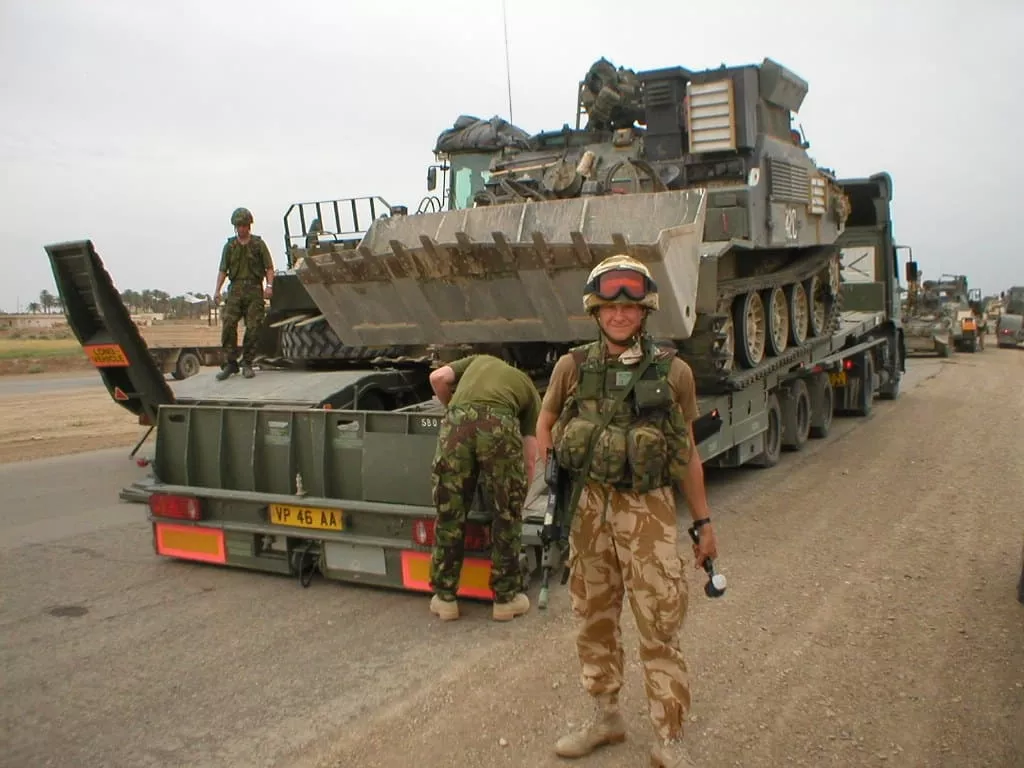
  • Single, Tandem & Tri-axle Articulated Trailers
  • Single, Tandem & Tri-axle Drawbar Trailers
  • Sliding Bed Trailers
  • Twin & Tri-axle Ackerman Steer Trailers
  • Heavy-Duty Ackerman Steer Engine Transporters
  • Bespoke Step-frame Trailers
  • Heavy-Duty Special Purpose Trailers
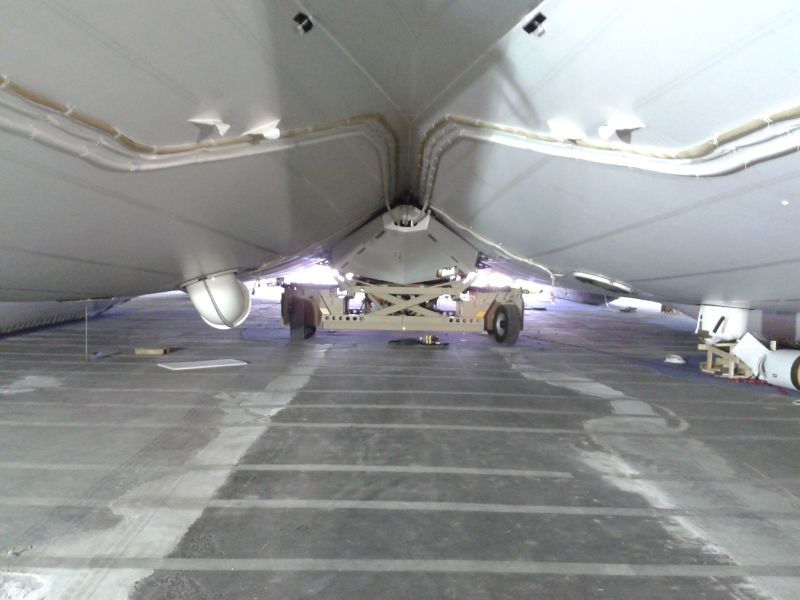
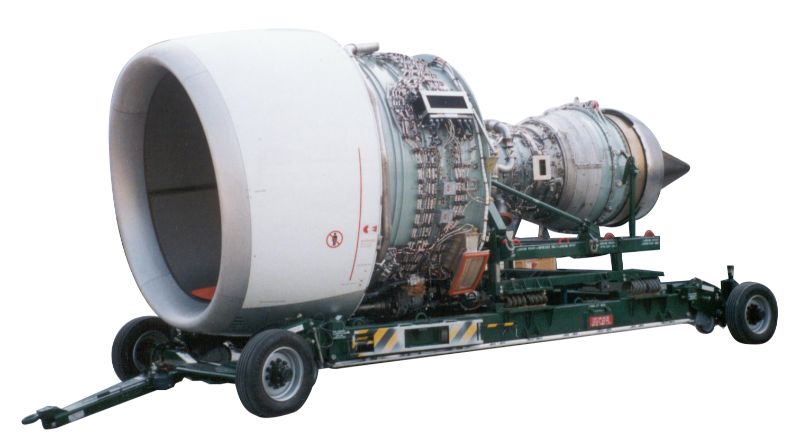
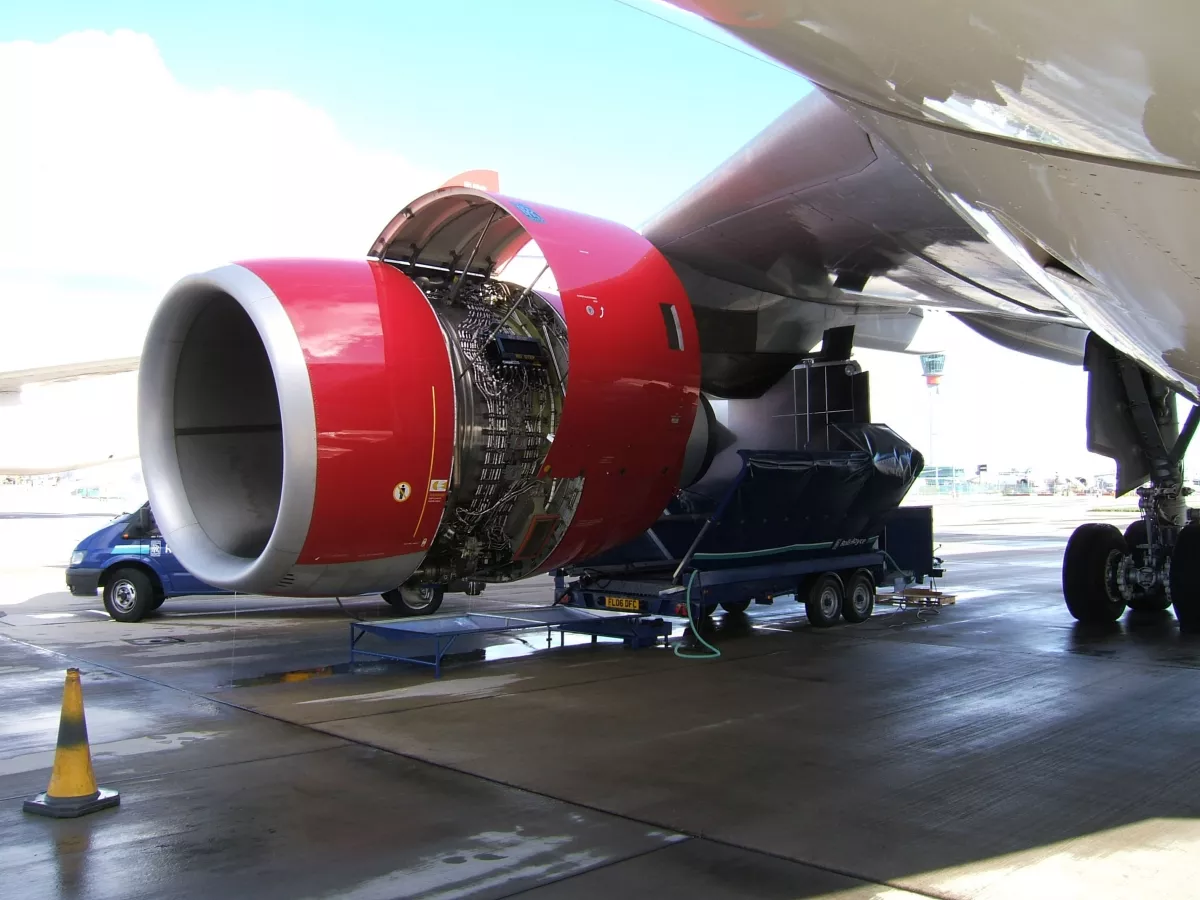
  • Aero-engine Transporters
  • Mobile Aero-Engine Test Trailers
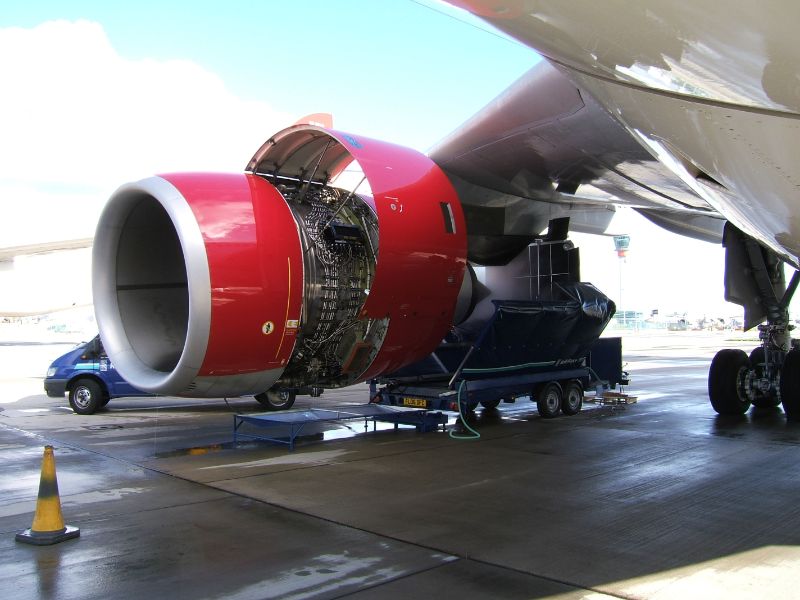
  • Mobile Aero-Engine Servicing Trailers
  • Aircraft Servicing Trailers
  • Turntable Runway Logistics Trailers
  • Shallow Loading Forklift Trailers
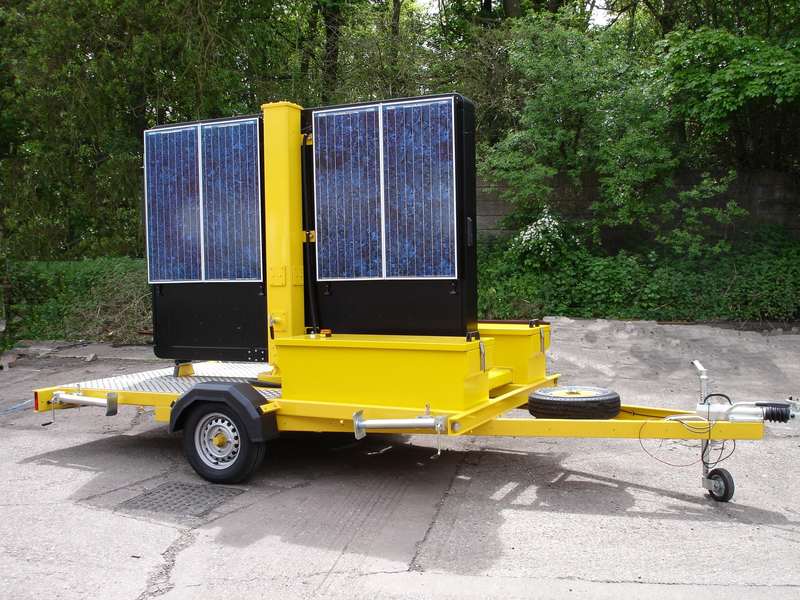
  • Roadside Traffic Information Trailers

Ancillary Equipment & General Engineering

Oldbury UK supplies a wide range of ancillary equipment and general engineering capability across all the market sectors and industries it serves.  To meet the very specialist requirements of the defence and homeland security sector, this capability also includes equipment for extreme temperature, climate and environmental conditions, ballistic protection and CBRN operations.

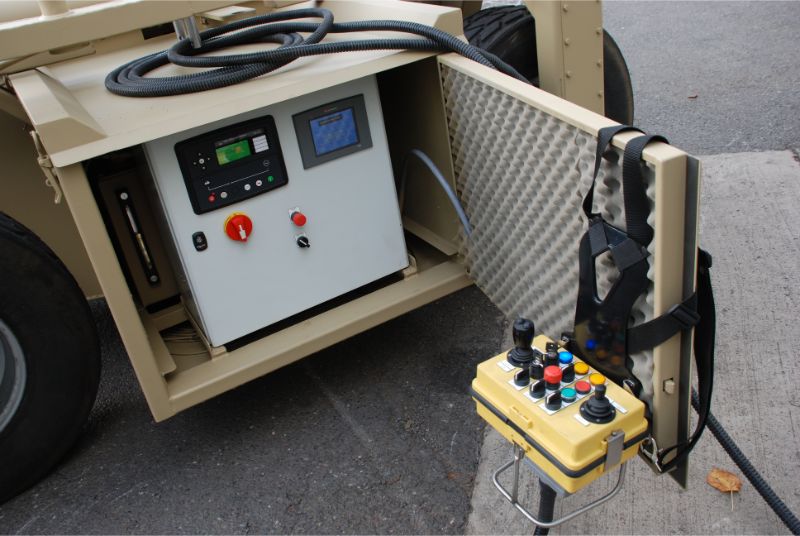
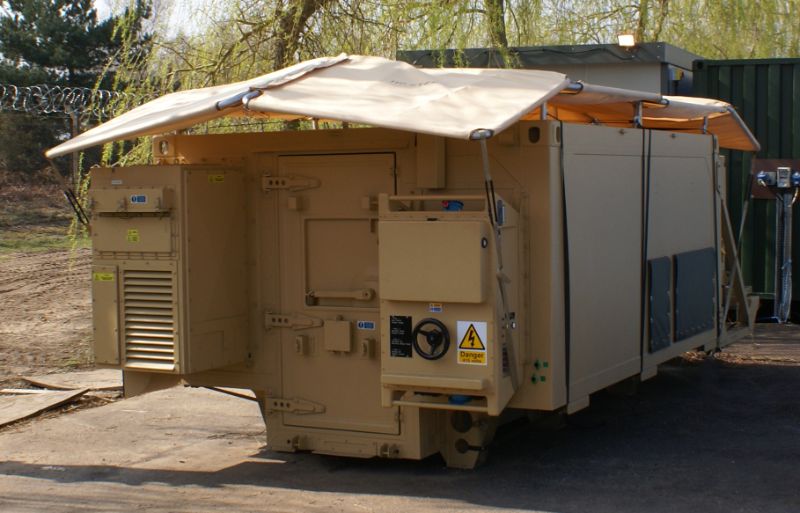
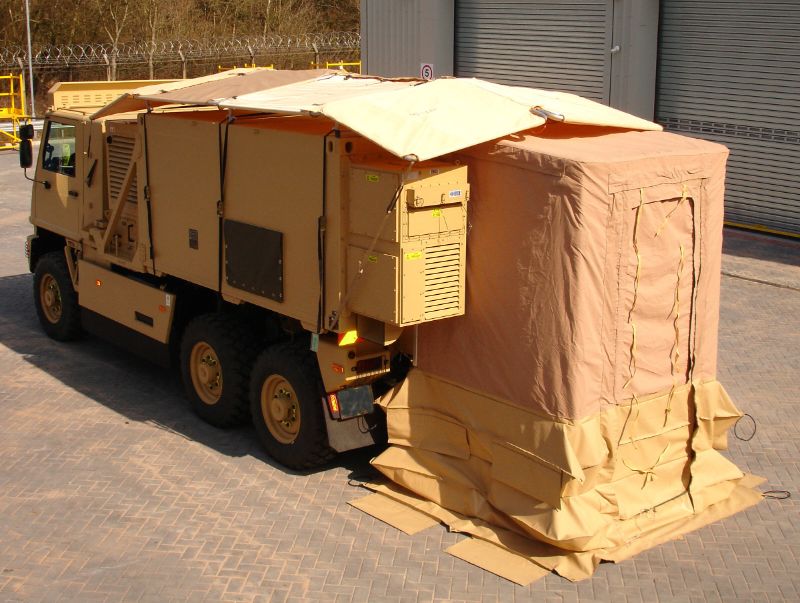
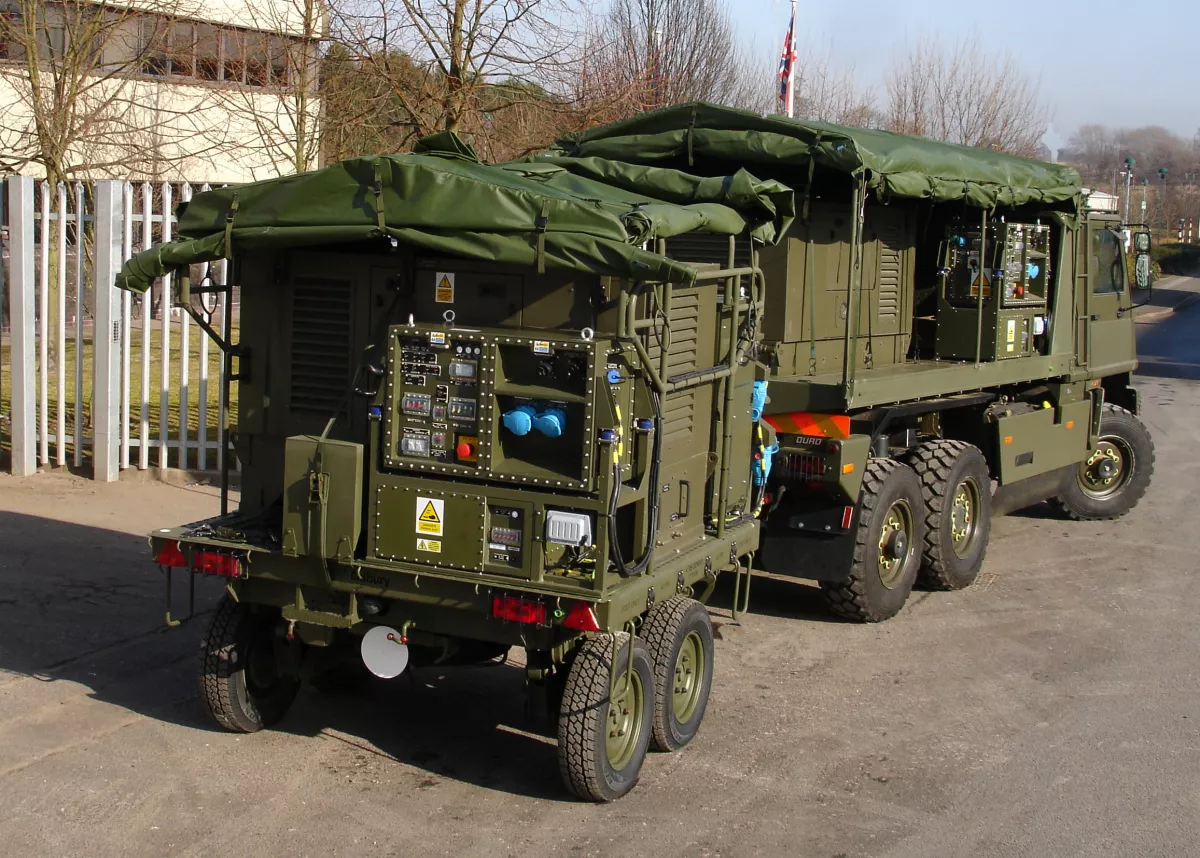
Oldbury’s range of compact, high performance generator sets is available either for self-standing, trailer-mounted applications – or fully integrated as part of much larger land systems.  The company’s heat and solar protection systems are successfully managing extremes in temperature fluctuation, enabling sensitive electronic equipment to operate close to ambient conditions.  Oldbury environmental shelters and enclosures effectively shield the entry and exit areas of containers and operating units from dust ingress and other contamination which could otherwise compromise reliability.

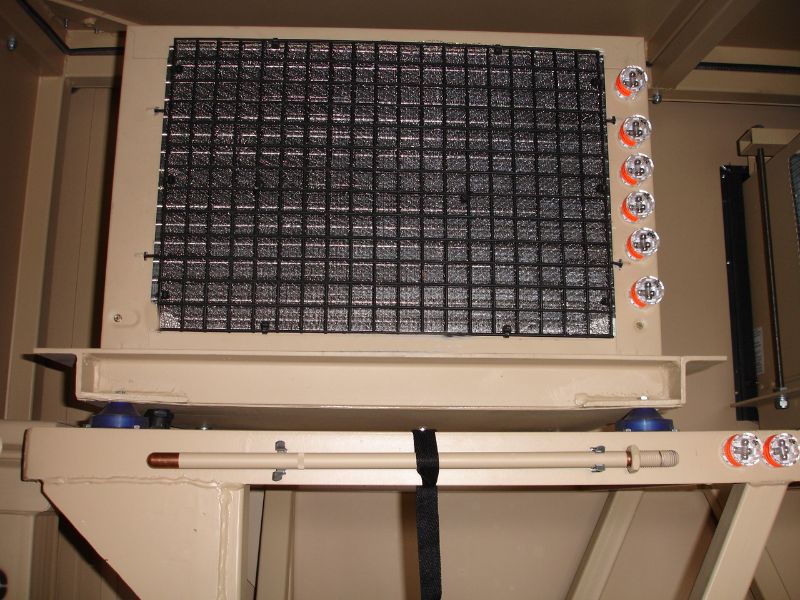
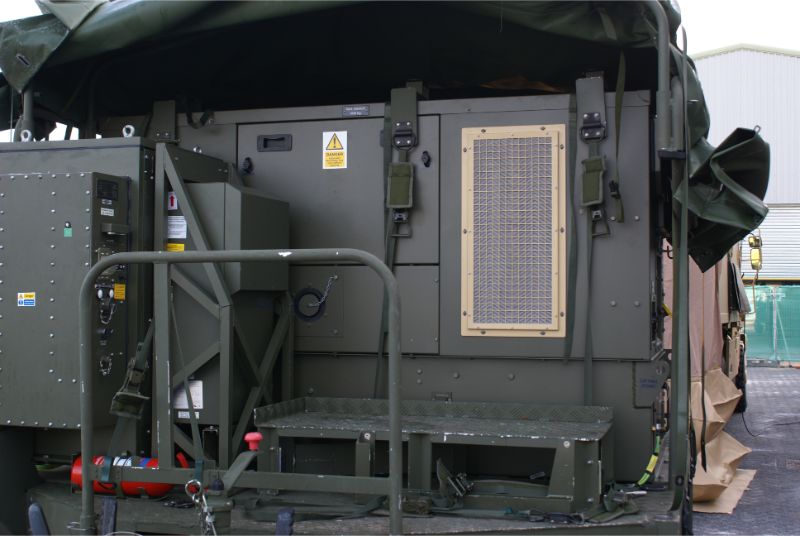
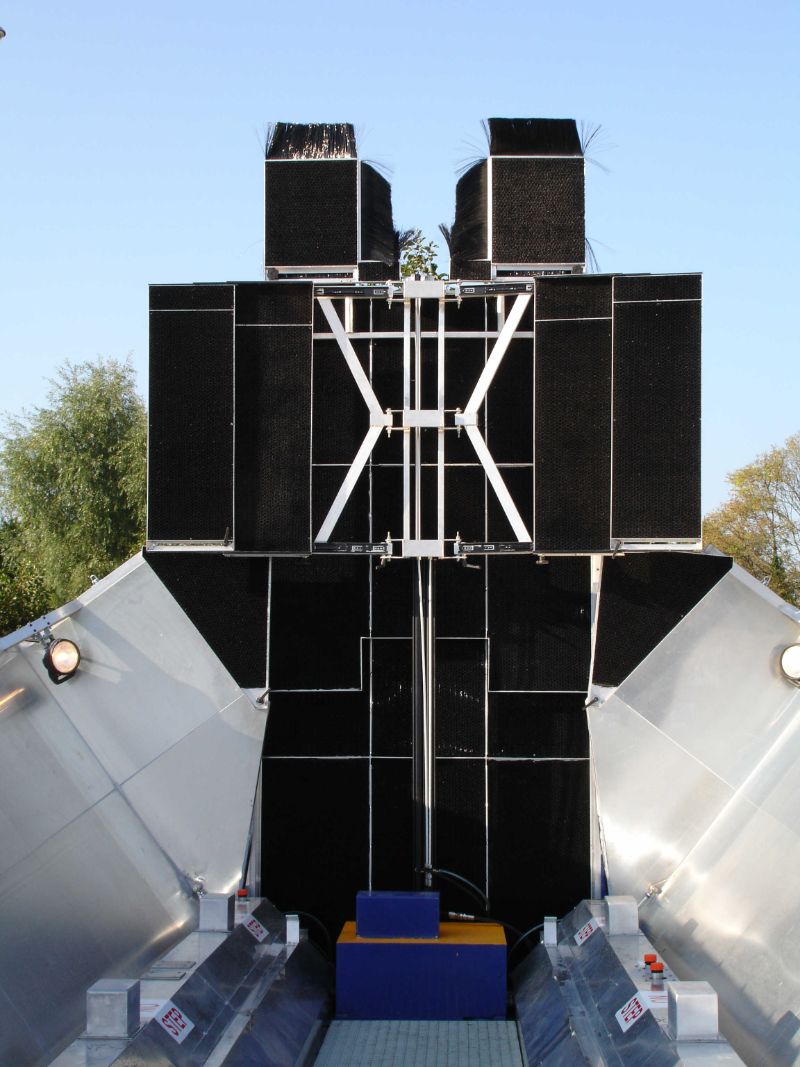
Oldbury has also designed and manufactured a range of high performance filtration systems, both for new equipment and for retrofit to existing in-service units.  The systems achieve high volume airflow whilst efficiently scavenging dust and other particulate matter which could otherwise impact on equipment performance.

Oldbury air conditioning and climate control systems are designed to operate in extreme conditions and are suitable for installation in new shelters and containers, as well as panel or window retrofit within existing units.

Requirements for which Oldbury has provided engineered solutions include:-